Backpack Size & Capacity Guide: 20L, 30L, 40L+
Discover how to run a custom backpack oem program for EU & US: materials, tech pack, sampling, QC and shipping. Get OEM/ODM-ready checklists and quote guidance.

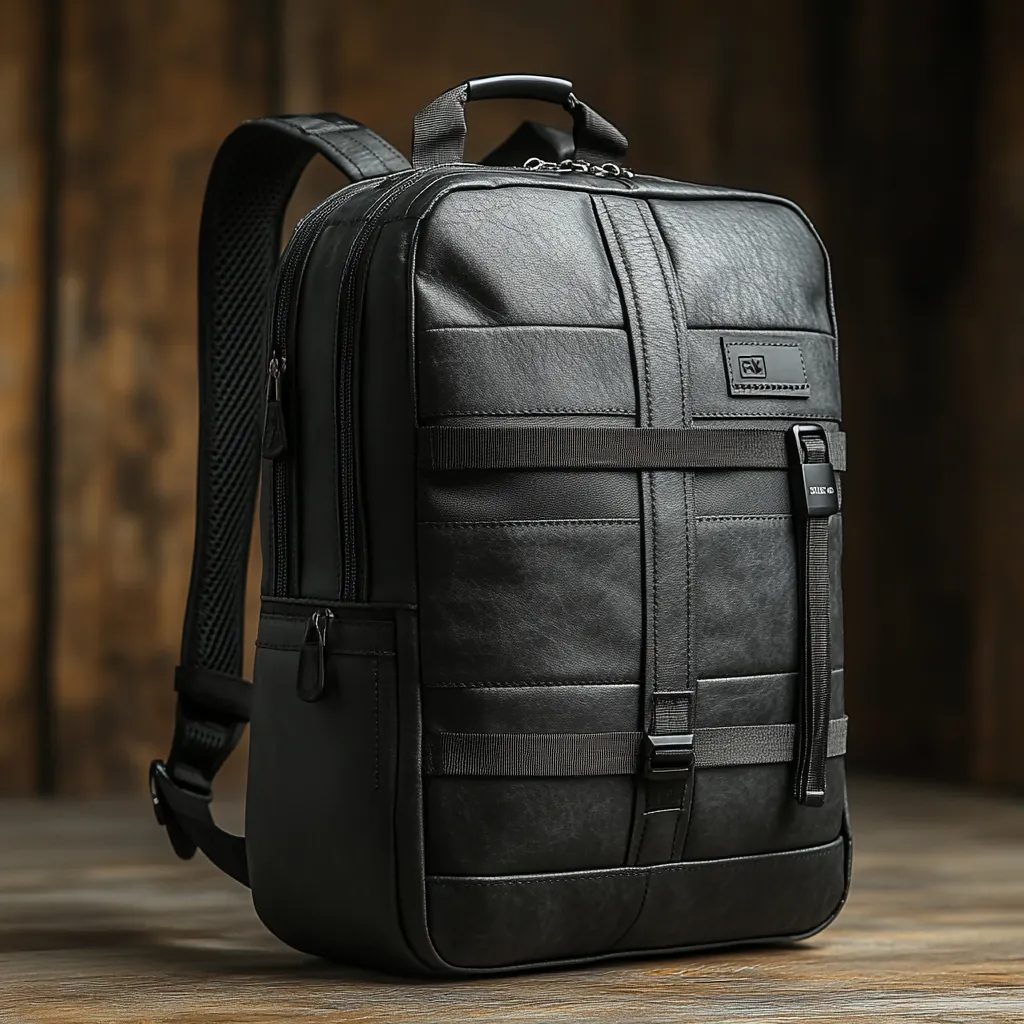
Inside the Build: How a Backpack Goes From Pack to Carton
If you are targeting EU & US with a premium positioning, the key is to prevent variance: materials, trims, workmanship and packout rules must be written and checked.
Control points the build is measured against
- 15+ years experience in custom sports & outdoor bag manufacturing
- ISO 9001 & BSCI certified professional OEM/ODM manufacturer
- Free professional design & 3D rendering service
Buyers often judge factories by “nice samples”. That is not enough. Genuine differentiation lies in output uniformity between runs, plus reliable defect suppression and adherence to agreed delivery windows.
Any tour worth taking is a control-point checklist in disguise, not a showroom trip.
Stage-by-stage: how the order is worked
- Brief alignment: settle the claim scope, cost target and packing rules before any sample.
- Within material sourcing, lock by spec: coating/laminate spec, fabric route, trim vendors.
- Pattern control: build templates, set a tolerance map, plan the reinforcement.
- Cutting stage: check grain direction plus marker efficiency; hold shade lots steady.
- Sewing and welding: hold the line on stitch spec, seam allowance, critical-zone reinforcement.
- At the final assembly stage, placement jigs position logos, hardware and accessories.
- Close with inspection: AQL sampling, carton marks and the export paperwork.
Typical buyer use scenarios
- commute
- school
- travel
- corporate gifting
- outdoor activities
Key functions buyers request most
- laptop sleeve
- breathable back panel
- padded straps
- multi-compartment layout
- durable zippers
Choosing the Best Materials for Custom Backpacks
Material choice is not just “fabric”. A build route means shell, coating/laminate and lining, seam strategy, then closures. Advertising assertions together with cost objectives fix what the lowest acceptable process looks like.
Your short list should hold 1–2 entries from the table underneath, each later validated by sampling and ISO/AATCC/ASTM procedures.
| Material | Performance | Cost Range | Leading For | Upsides & Watch-outs | Risks & How to Control |
|---|---|---|---|---|---|
| PU coated polyester (600D, per the specification) | Good repellency (ISO 4920 / AATCC 22 per spec); moderate barrier (ISO 811 to spec) | US$1.2–6.0 / meter (per the specification) | Value/core lines where print clarity matters | Upsides: cost controlled. Trade-offs: coating wear over time | Define spray rating targets and scuff resistance benchmarks; protect high-wear zones |
| Recycled RPET (route, to spec) | Sustainability positioning; performance depends on coating/laminate (ISO 4920 / ISO 811 as specified) | US$1.5–3.8 / meter (per the specification) | Eco positioning programs and corporate procurement | Merits: sustainability narrative. Watch-outs: supply stability and lot drift risks | Lock supplier lots, traceability and color delta; validate print and coating compatibility |
| Canvas / cotton (per spec) | Good hand-feel and print; waterproofing depends on finish (AATCC 22 per the specification) | US$1.0–3.5 / meter (as specified) | Retail lifestyle lines, totes and promotions | Upsides: classic look. Watch-outs: heavier; stain risk without finish | Define shrinkage and colorfastness tests (AATCC 61 / ISO 105 per the specification); specify lamination if needed |
Narrowing the material route quickly
- Work back from use: where it rubs, where it carries load, and how wet it gets set the route.
- Decide whether the claim covers the whole bag or only zones like the main compartment.
- Every referenced ISO/AATCC/ASTM procedure should be listed, together with the numeric bar for approval.
- Choose route-suitable trims, from zipper type and sliders to buckles and webbing strength.
- Confirm that print and branding suit the specified fabric.
- Scuffing and creasing usually trace to transit, not to stitching defects.
Per factory note, the tech pack must carry test references labelled by spec. Fail to do this and the supplier cannot manage pass criteria; “waterproof” ends up disputed instead of specified.
Begin compliance planning early for EU/UK or regulated-channel sales; material restrictions and labeling rules must be defined by spec. Last-chance repairs to packaging and trim never become necessary.
Design and Development: How the Build Is Specified
A nice sample means little when packaging rules, tolerances, the stitch spec, the BOM and the test method remain unset in the tech pack. The outcome is uneven bulk output plus flaws nobody expected.
Tech pack contents that get a fast quote
- Artwork files: vector format, color codes, size, and placement coordinates
- Measurement table: critical dimensions and tolerances by zone
- Trims and hardware specs: zipper type and size, slider, buckle strength class, metal vs plastic
- Packaging spec: insert, polybag, carton count, carton marking, barcode placement
- Testing plan: references and pass criteria (ISO/AATCC/ASTM as specified)
- Revision control: version number, change log, and approval record
The development sequence, as it really runs
- Pin down who buys it, at what retail band, and where it sits.
- Confirm the claim scope and its test plan by spec.
- Artwork placement, tolerance map, measurement table and BOM: four pieces that make the tech pack.
- Fit, structure and material route get validated at prototype sampling.
- Final BOM, final packaging route: the PP stage.
- Sign-off requirement: QC checklists plus the reference sample, ahead of bulk cutting.
Sample-stage checks that prevent expensive rework
- Confirm fabric shade and coating feel with the actual supplier lot (per the specification).
- Open, close and repack the product many times, watching for corner wear and seam creep.
- Three things need checking per lane: rub marks, folding lines, and defence against humidity.
- One PP sample, built with the final BOM and final packing route, is what needs approval.
- Lock all changes before bulk cutting; avoid late feature creep.
Fewer sample rounds: what actually helps
- Flexible MOQ for small brands & corporate orders
- Sampling: 6-10 working days for standard builds, 12-15 for complex construction
- Global shipping: FOB, CIF, DDP available
Why a repeatable build outperforms a hero sample
Success example (anonymized): a premium program targeting EU & US reduced rework by freezing a single tech pack, running one pre-production sample using the final BOM, and aligning QC checkpoints before cutting. A construction that can be duplicated means each season's reorder goes to the same partner.
Production & Manufacturing Methods for Backpacks
Manufacturing method selection depends on silhouette and performance targets. In most programmes, the winner picks construction that is at once simplest, repeatable and claim-scope compliant.
Weigh MOQ requirements against turnaround duration and price tier using the options table.
| Production Type | Lead Time | MOQ | Cost Level | Leading For |
|---|---|---|---|---|
| ODM catalog customization | 6-10 working days + 35-50 days | low–medium (to spec) | low–medium | Fast launches and proven silhouettes |
| Small-batch pilot run | 6-10 working days + 35-50 days | 500 pcs | medium | Startups, corporate gifting, SKU validation |
| Standard OEM mass production | 35-50 days | medium–high (to spec) | optimized | Retail replenishment and stable demand |
| Expedited production program | 15–25 days (to spec) | by program | higher | Time-critical launches |
Build methods worth naming in the pack
- Seam construction and reinforcement mapping (anchors, corners, zipper ends, base wear zones)
- Bonding / lamination requirements and peel strength targets (as specified)
- Foam thickness and density for structure (as specified)
- Stitch density and thread type for load zones (to spec)
- Edge binding method and tolerance for clean finishing
If you want to move from ODM to full OEM, lock the BOM and measurement tolerances first. Uniformity across bulk runs hinges on this step.
Defects pile up fast at bulk scale. Do not expect end inspection to trap everything; earlier interception at inline QC is the safer path.
Branding and Final Assembly
Branding fails when placement rules are vague. Sign off a proof printed on the final material, and hold placement to templates so nothing drifts.
Premium logo packages covering rubber patches, embroidery, custom pullers and metal logos require acceptance criteria early; per spec, the color delta, then edge sharpness and misalignment tolerance.
Decoration routes available (pick one or two per SKU)
- Screen print / heat transfer (best for clean graphics and scale)
- Embroidery (premium look, confirm stitch density and backing)
- Custom zipper puller / metal logo (premium trims, longer lead time)
Closing-stage checks that cut return rates
- Brand mark alignment check against placement template
- Metal parts function check: buckles, sliders, and snaps
- Zipper end reinforcement and smoothness check
- Visual check for wrinkles, creases, and surface scuffs before packing
Freight, Documents and Delivery
Shipping is part of product quality. Identical builds split into flawless or faulty purely through how packing is specified, box strength chosen, and moisture handled.
Shipping under DDP, CIF, or FOB terms is possible. Nothing should reach the floor until compliance, labelling and barcode requirements are agreed; that is how cartons stay retail-ready.
Checkpoints on the shipping leg
- Confirm packaging spec (inner polybag, inserts, carton marking).
- Assess how the item fares when dropped or pressed.
- Warehouse scanning depends on locked labeling, barcodes and carton counts.
Sell through Amazon or major retailers and packaging plus labeling is often why goods get rejected first. Formalise carton requirements instead of improvising near the finish line.
Key Factors to Choose a Reliable Backpacks Manufacturer
Choosing a supplier is risk management. Where a factory is reliable, process control shows up as material inspection, inline QC and pre-shipment inspection governed by your acceptance criteria.
Use this checklist before signing an OEM/ODM contract for backpacks.
Partner selection checklist
- Will they price off your pack and show what they assumed?
- Are alternatives by spec offered, and BOM sourcing controlled by them?
- Do they evidence QC checkpoints, IQC to IPQC to FQC, and an AQL plan?
- Without hurting workmanship, can they allow a flexible MOQ?
- Can they give firm lead time commitments and a defined escalation path?
- Do they bring packaging and shipping know-how that fits your market?
What to verify when you walk the production site
- Incoming material inspection records and traceability by lot
- Inline QC stations and sampling frequency
- Measurement tools calibration and template storage
- Packing area: carton marking, barcode process, and SKU separation
- Corrective action loop: how issues are documented and closed
- Load space reality: line balance, overtime policy, and peak season plan
Where this build route is strongest
- Strong at structured bags: stand bags, hard-base bags, specialized tooling
- Multi-stage QC system: incoming material → inline → pre-shipment
- Sustainable options: RPET, recycled nylon, eco-friendly fabrics
Matching Litres to Load: The Numbers Behind 20, 30 and 40 Litres
Capacity is only useful if the frame behind it can carry the weight that capacity implies. A 20 litre daypack and a 40 litre travel pack differ in more than volume: shell denier, empty weight, strap width and back panel length all have to move together, and the table below gives the pairings our production team uses when a buyer sends a sketch with a litre figure but no specification. Treat the empty weight column as a target to design against, because every 100 grams saved on the shell is 100 grams of payload the user can carry.
| Nominal capacity | External dimensions (cm) | Empty weight target | Comfortable load |
|---|---|---|---|
| 20 litres | 42 x 28 x 18 | 450-600 g | 4-6 kg |
| 30 litres | 48 x 32 x 22 | 700-950 g | 6-9 kg |
| 40 litres | 55 x 35 x 25 | 1,000-1,400 g | 9-12 kg |
| 50 litres and above | 60 x 38 x 28 | 1,400-1,800 g | 12-15 kg |
The comfortable load column is the one buyers ignore and users feel. A 40 litre body filled to 12 kg puts roughly 25 percent of body weight on an average adult frame, which is the point at which a hip belt stops being a feature and becomes a requirement. Note also that these dimensions are external: a bag quoted at 30 litres from external dimensions may hold nearer 26 litres by bead displacement, which is why the measurement method belongs in the specification alongside the number.
Sizing Rules That Decide Whether the Volume Is Usable
A bag can hold the stated litres and still be uncomfortable, because usable volume depends on how the load is carried rather than how much space exists. Check these six items before the pattern is graded.
- Back panel length should track torso: 38-45 cm suits a 20 litre daypack, 45-50 cm suits a 40 litre travel body, measured from the seventh vertebra to the iliac crest.
- Shoulder strap width scales with load: 25 mm webbing is adequate below 25 litres, 38 mm above 35 litres, with foam no thinner than 8 mm at the contact point.
- Add a hip belt once the expected load passes 7 kg, at 40-50 mm width, and check that it sits over the iliac crest rather than the waist.
- Set load lifters at a 30-45 degree angle from the top of the shoulder strap, which is the range that actually pulls the load toward the back.
- Pack the heaviest item within 10 cm of the back panel and centred, because weight held away from the spine multiplies the felt load.
- Confirm packed volume before booking freight: a flat-packed unstructured body can roughly double carton density against a framed one.
Sampling for a new size runs 6-10 working days, 12-15 where a frame sheet or moulded panel is involved, and bulk runs 35-50 days. Component options are listed under backpack materials, and fit tolerances are covered in the programme guide.
Frequently Asked Questions (FAQs)
What is a realistic MOQ for backpack OEM?
Material route, branding package and trims set the cost. The MOQ is 500 units, and MOQ terms are adapted for corporate accounts and low-volume labels.
How do we quote you without guesswork?
Quote inputs: a tech pack or sample to reference, fabric and finish target, logo application, quantity per colour, packaging requirements with FOB, CIF or DDP terms.
Sampling then production: what is the typical duration?
Complexity and material availability mean sampling runs 6-10 working days while mass production occupies 35-50 days.
What keeps bulk-order quality under control?
Build QC around documented acceptance limits and the AQL plan, checking inputs at intake, workmanship inline, and product before it ships.
Does your scope include private label plus ODM?
Yes. Choose ODM and ready silhouettes to launch faster, or OEM for full customization. As your catalogue expands, the relationship can move from ODM-led builds to a fully OEM model.
How are confidential designs and IP kept safe?
Ownership of tooling belongs in a separate agreement, technical files need version numbers, and an NDA protects disclosure. Stage-gated distribution plus a permissions check: share narrowly, then verify who can open things.
Is eco-friendly material in your range?
Yes. You can choose RPET or recycled nylon, aligned with performance targets and supply stability.
Would you send cargo DDP into our warehouse?
Yes. FOB, CIF, DDP: route availability follows the destination and its compliance requirements.
Further Reading and Internal Resources
Internal resources
Related blog posts
- Waterproof Dry Sacks: Sizing Guide for Manufacturers
- Waterproof Duffel Bags for Travel: Best-Selling Designs
- Waterproof Bag Trends 2026: Lightweight & Durable
- Waterproof Coatings for Bags: DWR, TPU & PVC Lamination
- Webbing Materials for Bag Straps: Nylon & Polypropylene
- What Brands Should Check Before Signing an OEM Bag Contract
Next step
Need a quote or sampling plan? Reply contents once we get your tech pack or reference photos: OEM/ODM options first, then lead-time plan and structured RFQ checklist.
• Lock keyword and claim scope for custom backpack oem
• Build a tech pack with BOM + tolerance map
• Choose materials route and validate tests (by spec)
• Plan sampling gates (lead time 6-10 working days)
• Set MOQ and cost targets (MOQ 500 pcs)
• Define QC plan and AQL checkpoints
• Confirm production + shipping timeline (25–35 days)
Ready to move on your next build?
Send over your requirements; a manufacturing plan and structured RFQ checklist are prepared for you.
Next guides: custom backpacks.
Two Factories Can Quote the Same 30 Litres and Be Four Litres Apart
Capacity is a measurement method before it is a number.
There are three ways to arrive at a litre figure and they disagree. Filling a bag with 20 mm beads and measuring the volume gives the highest number, because beads pack into corners. Multiplying external dimensions gives a higher number still, since it counts the space inside the foam and the lining. Displacement of a calibrated volume, or simply packing the bag with the things a user actually carries, gives the lowest and most honest figure. When you compare quotes, ask which method was used, because a 30-litre claim from one supplier and a 30-litre claim from another Structure eats capacity. A padded laptop sleeve, a moulded back panel and a reinforced base each consume volume that external dimensions do not account for, which is why a heavily featured 30-litre bag holds less than a plain one of the same nominal size. If capacity is a selling point, decide how much structure you are willing to pay for in litres, and state capacity as usable volume rather than as a nominal figure on the hangtag. can describe bags that differ by more than ten percent.
| Band | Typical dimensions | Empty weight | Realistic contents | Buyer note |
|---|---|---|---|---|
| 18–22 L | 42 x 28 x 16 cm | 0.45–0.70 kg | Light layer, 13-inch device, bottle | Day use, lowest freight cube |
| 26–32 L | 46 x 31 x 20 cm | 0.70–1.10 kg | 15-inch laptop, lunch, gym kit | Core commute size |
| 34–40 L | 50 x 33 x 24 cm | 1.00–1.40 kg | Laptop plus overnight clothing | Check airline sizer limits |
| 40 L and above | 55 x 35 x 28 cm | 1.30–1.90 kg | Two to three days of clothing | Cabin limits vary by carrier |
Choosing between bands is easier with a rule than with a chart. If the bag's heaviest regular load is a laptop and a light layer, 20 litres is correct and anything larger just encourages overpacking, which shows up as strap pain and returns. If it must carry a laptop plus a change of clothes or gym kit, 30 litres is the band that sells, because it still passes most workplace dress codes and still fits under a seat. Above 34 litres you are in travel territory, and the decision shifts from capacity to airline compliance.
Cabin limits are the constraint that catches programmes out. Most carriers publish a linear dimension limit and a weight limit, and the two together usually cap a backpack somewhere between 34 and 40 litres depending on how flat it is built. A bag designed to sit close to the back passes a sizer that a deeper, rounder bag of the same volume fails. If travel is part of the positioning, build the depth down and the height up, and state the airline claim on the hangtag Empty weight is the number users notice second, after comfort. A day bag above roughly 0.9 kg reads as heavy before it is packed, and a travel pack above about 1.6 kg starts to eat into the airline allowance that matters most on the return leg. Setting an empty-weight target in the brief forces material decisions early, and it is far easier to hit than to retrofit once the pattern is cut. only after testing it against a real sizer.
Capacity also drives freight, which is where size silently changes your landed cost. A 20-litre day bag nests tightly and fills a 20GP of roughly 28 CBM efficiently; a structured 40-litre travel pack with a moulded panel does not, and the same container may hold half the unit count. That difference is invisible in the unit price and obvious in the freight quote, so it is worth modelling Consider whether the programme needs one size or a family. A family of three sizes shares a bill of materials and spreads tooling, but each size counts as a style against the 500-unit minimum, so a three-size launch is three commitments. Where volume is uncertain, launch the middle size first and add the others once demand is known, reusing the approved materials so the existing testing stays valid. before the size is frozen rather than after.
Commercially, minimums are 500 units per style per colour and each size in a family counts as a style, so a three-size launch is three commitments unless you consolidate the bill of materials. Samples return in 6–10 working days, or 12–15 where a moulded panel is involved. If you are choosing between a commute and a travel programme, custom laptop bags and custom travel bags show how the two families differ in construction.