Sling Bags & Crossbody Bags: Hot Selling 2026 Styles
Learn how to run a custom sling bag oem program for North America: materials, tech pack, sampling, QC and shipping. Get OEM/ODM-ready checklists and quote
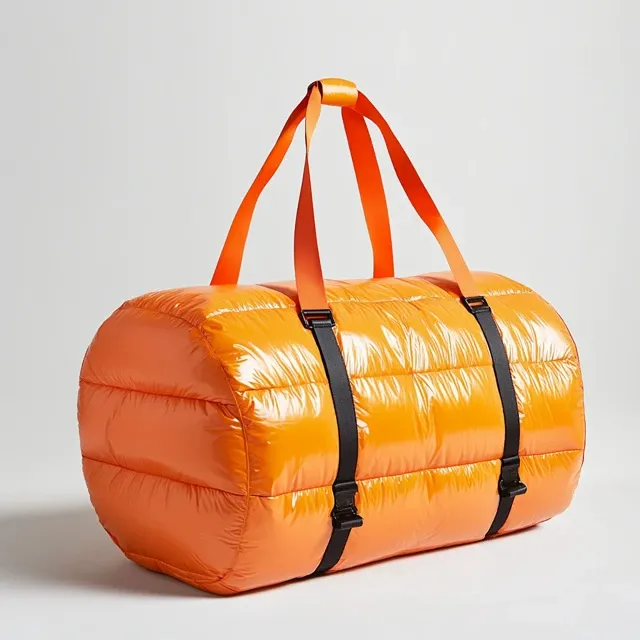
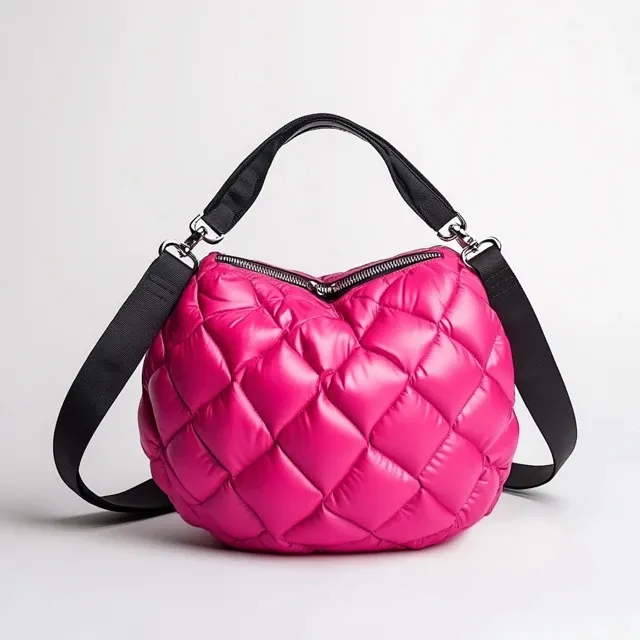
Where a Sling Bag Gets Made, and How It Moves
A professional sling bag program is a controlled workflow: clarify requirements, lock the build route, validate with measurable gates, then scale production with repeatable QC.
Primary SEO focus: custom sling bag oem. Secondary: sling bag manufacturer, private label bags, custom logo bags, OEM ODM bags.
The checkpoints that decide whether bulk runs
Any tour worth taking is a control-point checklist in disguise, not a showroom trip.
How the line handles your SKU
- Lock claim scope, price target and carton rules, and only then sample.
- Within material sourcing, lock by spec: coating/laminate spec, fabric route, trim vendors.
- Pattern work: cut templates, define tolerances, plan the stress-point build-up.
- Cutting stage: check grain direction plus marker efficiency; hold shade lots steady.
- Sewing and welding: hold the line on stitch spec, seam allowance, critical-zone reinforcement.
- At the final assembly stage, placement jigs position logos, hardware and accessories.
- Finish on AQL sampling, correct carton marking and complete documents.
Typical buyer use scenarios
- brand launches
- wholesale programs
- corporate procurement
- retail distribution
Key functions buyers request most
- custom sizing
- durable construction
- logo branding options
- retail-ready packaging
- consistent QC
Choosing the Best Materials for Custom Sling Bags
| Material | Performance | Cost Range | Leading For | Advantages & Limitations | Risks & How to Control |
|---|---|---|---|---|---|
| nylon | Even-handed durability (ISO 13934 tensile per the specification); good abrasion resistance (ISO 12947 per spec); stable for branding | US$1.6–5.5 / meter (as specified) | Main line items with predictable yield | Advantages: versatile. Trade-offs: performance depends on coating/finish | Lock coating spec, color tolerance and print compatibility; confirm reinforcement mapping |
| Recycled RPET (route, as specified) | Sustainability positioning; performance depends on coating/laminate (ISO 4920 / ISO 811 per spec) | US$1.5–3.8 / meter (to spec) | Eco positioning programs and corporate procurement | Advantages: sustainability narrative. Trade-offs: supply stability and lot drift risks | Lock supplier lots, traceability and color delta; validate print and coating compatibility |
| Canvas / cotton (as specified) | Good hand-feel and print; waterproofing depends on finish (AATCC 22 per the specification) | US$1.0–3.5 / meter (as specified) | Retail lifestyle lines, totes and promotions | Upsides: classic look. Watch-outs: heavier; stain risk without finish | Define shrinkage and colorfastness tests (AATCC 61 / ISO 105 to spec); specify lamination if needed |
Triage the material decision
- Decide from the field conditions: rubbing, carrying load and water drive the choice.
- Decide whether the claim covers the whole bag or only zones like the main compartment.
- Every referenced ISO/AATCC/ASTM procedure should be listed, together with the numeric bar for approval.
- Choose route-suitable trims, from zipper type and sliders to buckles and webbing strength.
- Confirm that print and branding suit the specified fabric.
- Scuffing and creasing usually trace to transit, not to stitching defects.
Design, Sampling and Sign-Off
The specification sheet that avoids a second round
Condensed here by design — the extended comparison belongs to own-brand programmes, alongside the rest of the reference data.
What happens first, second and third
- Write down the customer, the price tier and the role it plays.
- Confirm the claim scope and its test plan by spec.
- Artwork placement, tolerance map, measurement table and BOM: four pieces that make the tech pack.
- Fit, structure and material route get validated at prototype sampling.
- Final BOM, final packaging route: the PP stage.
- Sign-off requirement: QC checklists plus the reference sample, ahead of bulk cutting.
Getting the sample right first time
- Verify artwork location physically on paper before the selected print process runs.
- Load-test every anchor point: webbing, grab handles and D-ring areas, to specification.
- Review the zipper path, then slider feel, then the cycle requirement per spec.
- Open, close and repack the product many times, watching for corner wear and seam creep.
- Three things need checking per lane: rub marks, folding lines, and defence against humidity.
- One PP sample, built with the final BOM and final packing route, is what needs approval.
- Lock all changes before bulk cutting; avoid late feature creep.
Reducing back-and-forth before bulk
From first build to annual reorder
Success example (anonymized): a premium program targeting North America reduced rework by freezing a single tech pack, running one pre-production sample using the final BOM, and aligning QC checkpoints before cutting. A construction that can be duplicated means each season's reorder goes to the same partner.
Production & Manufacturing Methods for Sling Bags
Weigh MOQ requirements against turnaround duration and price tier using the options table.
Methods and the numbers behind them
Branding Methods and Final Build Steps
Choosing how to apply your logo
Keeping returns down at the last station
For the complete spec grid — including the acceptance criteria and lot sizes — read tote bag specifications.
Shipping Mode, Cost and Timing
The export sequence, gate by gate
Key Factors to Choose a Reliable Sling Bags Manufacturer
Use this checklist before signing an OEM/ODM contract for sling bags.
What to ask before you place volume
- Do they price the pack and flag every assumption they made?
- Are alternatives by spec offered, and BOM sourcing controlled by them?
- Do they evidence QC checkpoints, IQC to IPQC to FQC, and an AQL plan?
- Without hurting workmanship, can they allow a flexible MOQ?
- Can they give firm lead time commitments and a defined escalation path?
- Do they bring packaging and shipping know-how that fits your market?
What an audit should look at, line by line
Detailed thresholds, sampling levels and test references are consolidated on quality control and certification so one source stays current for every programme.
Where the value sits
Silhouettes that are anchoring current assortments
Three body types dominate range planning right now. The compact vertical sling, around 1.5 to 3 litres, carries phone, wallet and travel documents. The wide horizontal crossbody, roughly 4 to 7 litres, takes a tablet and a water bottle. The convertible belt-and-sling style serves travel retail and festival channels. Each has a different panel count, hardware set and price ceiling, so ranges work best when planned by role rather than by counting SKUs.
Construction follows from those roles. Vertical slings favour one main panel with a curved zipper, which keeps seam count low and suits coated and laminated face fabrics. Horizontal styles need a base insert and usually a divider, which raises labour minutes; unit cost rises faster than fabric area alone would suggest, and that difference should show in the costing rather than being discovered later.
Material separates channels. Certified recycled polyester and solution-dyed nylon serve promotional and travel-retail programmes; matte-finish ripstop is common in athleisure capsules; full-grain or bonded leather anchors higher price points. The same silhouette needs a rewritten tech pack for each of these, because seam allowance, reinforcement and hardware load change with material thickness.
Colour, hardware finish and building one assortment inside one minimum
Hardware finish is doing more differentiation work than colour in current assortments. Matte black, brushed gunmetal and soft gold read very differently under retail lighting even on identical fabric, and a finish change costs far less than adding structure or features. Lining colour is the second cheapest lever, seen at the moment of purchase and almost invisible in construction cost.
Colour planning should separate volume from experiment. Two core neutrals carry repeat orders across seasons; seasonal accents rotate and are the ones most likely to be discounted. Keeping both on the same nominated shell lets one order produce several commercial outcomes instead of committing a separate run to each colour.
| Role | Size band | Typical build | Main cost driver |
|---|---|---|---|
| Compact vertical sling | 1.5 to 3 litres | Single panel, curved zipper | Zipper curve and pull hardware |
| Wide horizontal crossbody | 4 to 7 litres | Structured base with divider | Labour minutes |
| Convertible belt sling | 2 to 4 litres | Webbing system with buckle | Hardware count |
Tooling decides how quickly development pays back. Stock hardware keeps sampling inside 6 to 10 working days and avoids tooling charges entirely. Custom buckle shapes or pressed panels extend that to 12 to 15 working days and carry tooling and screens at USD 300 to 2,500, which is sound when several styles share the component and poor when it serves a single season.
Lead time stays invisible until it becomes the constraint. Bulk production takes 35 to 50 days and sea freight adds 25 to 35 days, so a launch date is effectively settled several months ahead. Where the selling window is short, air freight at 5 to 8 days protects the calendar, and express at 3 to 5 days suits a re-order against proven demand.
Assortment economics are confirmed during quoting, and QUANZHOU JUNYUAN BAGS returns pricing within 24 to 48 hours. Programme structure is described in private label bags, and wear-side decisions sit in the sling ergonomics guide.
Frequently Asked Questions (FAQs)
Which sling silhouette sizes should anchor a first capsule collection?
Three bodies cover most demand: a vertical sling around 1.5 to 3 litres, a horizontal crossbody near 4 to 7 litres, and a convertible belt style. Each serves a different use case and price ceiling, so they compete far less with one another than three size variants of a single shape do.
How many colourways can be combined inside a 500-piece minimum order?
Several, provided the shell, lining and hardware stay common. The practical limit is cutting yield rather than piece count: very small colour runs force additional marker changes. Sharing construction across the colourways keeps unit pricing stable while giving the merchandising team genuine choice.
Does custom hardware tooling pay off for a mid-priced sling range?
It depends how many styles share the component. Tooling and screens cost USD 300 to 2,500 and are charged once, so cost per unit falls quickly when reused across a family. For a single body with one season of expected demand, stock hardware usually returns better margin.
Which fabric direction suits a promotional tier versus a premium tier?
Promotional programmes lean on certified recycled polyester or solution-dyed nylon for durability at controlled cost, while premium tiers use bonded leather or matte-finish ripstop. Each material needs its own pattern adjustments, so the saving sits in shared development time rather than in shared production.
How far ahead should a seasonal sling launch be locked?
Work back from roughly four months. Bulk production takes 35 to 50 days and sea freight adds 25 to 35 days. Where the selling window is short, booking air freight at 5 to 8 days protects the calendar, and express at 3 to 5 days suits re-orders made against proven demand.
Should one body be offered in more than one material?
Yes, where the versions sit at different price points instead of competing directly. Buyers often run a recycled polyester body for promotional channels and a leather version for speciality accounts. Each needs pattern adjustments, so the benefit is shared development rather than shared production.
What keeps two tiers of one sling design visibly different at shelf?
Hardware finish first, then lining and edge treatment. Matte black, brushed gunmetal and soft gold read differently under retail lighting on identical fabric, and finishes cost less than adding structure. A contrasting lining colour that only appears when the bag opens is another low-cost tier signal.
What sampling timeline applies to a convertible sling with a buckle system?
Sample fees run USD 50 to 150 and are refunded against the bulk order. A convertible design with a webbing system takes 6 to 10 working days; adding a moulded panel or a custom buckle extends it to 12 to 15. MOQ is 500 pieces and pricing returns within 24 to 48 hours.
Next Steps and Further Guides
Internal resources
- Request a quote (RFQ)
- Browse products & categories
- Download QC checklist
- Packing format specification guide
Related blog posts
- How To Choose Materials For Custom Tool Bag
- How To Choose Materials For Custom Waterproof Backpack
- How To Plan Lead Time For Custom Cosmetic Bag
- How To Plan Lead Time For Custom Cotton Bag
- How To Plan Lead Time For Custom Garment Bag
- How To Plan Lead Time For Custom Leather Goods
Next step
• Lock keyword and claim scope for custom sling bag oem
• Build a tech pack with BOM + tolerance map
• Choose materials route and validate tests (by spec)
• Plan sampling gates (lead time 6-10 working days)
• Set MOQ and cost targets (MOQ 500 pcs)
• Define QC plan and AQL checkpoints
• Confirm production + shipping timeline (25–35 days)

Let's scope your next order
Send over your requirements; a manufacturing plan and structured RFQ checklist are prepared for you.
Next guides: custom backpacks.
Six silhouettes carrying the category into 2026
The sling and crossbody category has consolidated into a small number of recognisable shapes, and the commercial question for a 2026 programme is not which shape is newest but which one your channel can actually sell at a margin. Volume, material and closure define the silhouette far more than decoration does, and each of the six shapes below has a different cost floor and a different buyer.
The micro sling at 1.5 to 3 L is the entry price point and the volume driver. It holds a phone, a card holder and sunglasses, it uses very little fabric, and it is the shape most often bought on impulse and in more than one colour. Because the marker is tiny, fabric yield is excellent and the unit cost is dominated by hardware rather than material, which means the cheapest upgrade that reads as premium is a better zip and a custom puller, not a better fabric.
The tech sling at 4 to 7 L is where the margin sits. It carries a tablet or a small laptop, needs a padded sleeve and therefore a structured panel, and justifies a higher price because it displaces a small backpack. Above that, the camera-style crossbody borrows its proportions from camera bags: a boxy body, a wide opening flap and a divided interior, which sells well to a demographic that likes the look without owning a camera. The crescent and half-moon body is the fashion-led entry, and it is the one shape where the pattern genuinely matters, because a curved top seam either drapes beautifully or puckers depending on how the panel is cut relative to the grain.
| Silhouette | Volume | Body material | Structure | Indicative FOB |
|---|---|---|---|---|
| Micro sling | 1.5 to 3 L | 300D RPET or nylon | Unstructured | 2.80 to 5.00 |
| Tech sling | 4 to 7 L | 600D with padded sleeve | Semi-structured | 5.50 to 9.00 |
| Camera crossbody | 5 to 9 L | Waxed canvas or 900D | Structured | 7.00 to 12.00 |
| Crescent body | 3 to 6 L | Recycled nylon, quilted | Unstructured | 5.00 to 9.00 |
| Quilted chain crossbody | 2 to 4 L | PU or recycled leather | Light structure | 6.00 to 11.00 |
| Waist-to-crossbody | 2 to 5 L | Ripstop nylon | Unstructured | 3.50 to 6.50 |
Picking a shape for your channel, and what it costs to change your mind
The decision rule is simple. If your channel is gifting, promotional or impulse retail, take the micro sling or the waist-to-crossbody format and spend the budget on colour breadth rather than on construction, because those shapes sell in multiples. If your channel is a brand store or a premium marketplace, take the tech sling or the camera crossbody, because the structured panel and the divided interior are what the customer is paying for and they tolerate a higher price. If your channel is fashion-led, the crescent and quilted bodies win on look and lose on function, and that is acceptable as long as the product copy does not promise organisation the shape cannot deliver.
Material choice moves the price more than silhouette does within this category, because the fabric area is small. A recycled leather or a waxed canvas can double the material line against a 300D RPET on the same pattern, and that is a larger swing than any construction change. Hardware is the second lever, and on a small bag it is a visible proportion of the unit: a branded metal puller and a magnetic closure can add a dollar or more, which on a 3 L bag is a meaningful fraction of the FOB price. Tooling for a custom puller or a magnetic closure housing sits in the USD 300 to 2,500 band, and it amortises well across a 500-unit run but poorly across a 200-unit test.
Schedule around the sampling window rather than the season. Sampling takes 6 to 10 working days on an existing silhouette and 12 to 15 where a new curved seam or a structured sleeve is being developed, then mass production runs 35 to 50 days after approval, and sea freight at 25 to 35 days means a six-month lead from first sample to shelf is the realistic planning figure. Air at 5 to 8 days compresses the back end at a cost that usually only makes sense for a launch drop. Our production team quotes in 24 to 48 hours at 500 units per style and colour, with 300 discussable on repeats. Shape and material options are covered in the materials reference and the pricing mechanics in the cost and MOQ guide; wear comfort for these formats is analysed in sling ergonomics.
Numbers age badly when copied into dozens of places, so the maintained version of this grid stays on quality control and certification.
Rather than repeat the same matrix here, keep the detailed grading with the central reference on material selection — it lists the acceptance numbers and sampling levels our team works to.