Pattern Making Basics For Custom Duffel Bag
Learn how to run a custom duffel bag oem program for United States: materials, tech pack, sampling, QC and shipping. Get OEM/ODM-ready checklists and quote
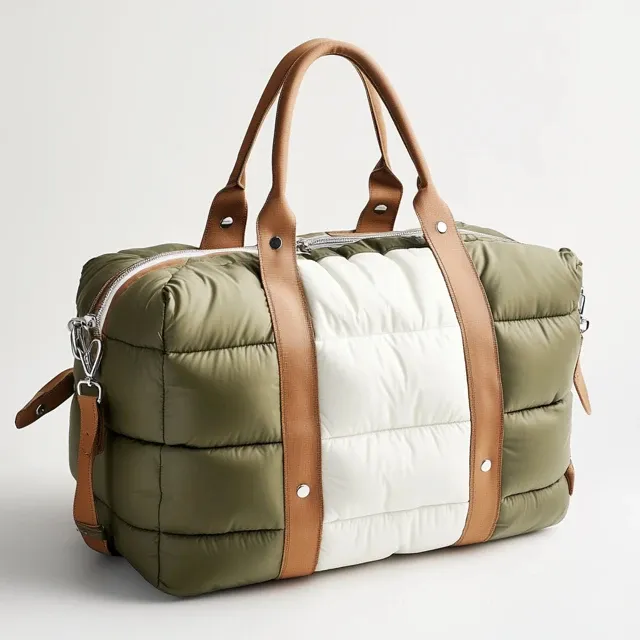

From Pattern to Pallet: Building a Duffel Bag
A professional duffel bag program is a controlled workflow: clarify requirements, lock the build route, validate with measurable gates, then scale production with repeatable QC.
Primary SEO focus: custom duffel bag oem. Secondary: duffel bag manufacturer, private label bags, custom logo bags, OEM ODM bags.
What is held to a number, and who signs it
Where you need the granular row detail, handbag specifications carries it with the test methods and sample sizes attached.
A serious walkthrough follows the paperwork from incoming fabric to sealed carton.
Walking the order through seven stations
- Align on what is claimed, what it costs and how it packs before sampling starts.
- By spec, material sourcing locks the coating/laminate spec, fabric route and trim vendors.
- Make the patterns, agree tolerances and decide the reinforcement layout.
- Manage dye lots, and verify marker yield plus grain alignment while cutting.
- Reinforcement at stress points, then seam and stitch specs applied at the station.
- Fixtures hold placement while hardware, logos and accessories go on.
- Then inspection and packing: AQL draws, carton marks, export papers.
Typical buyer use scenarios
- brand launches
- wholesale programs
- corporate procurement
- retail distribution
Key functions buyers request most
- custom sizing
- durable construction
- logo branding options
- retail-ready packaging
- consistent QC
Choosing the Best Materials for Custom Duffel Bags
| Material | Performance | Cost Range | Preferred For | Merits & Watch-outs | Risks & How to Control |
|---|---|---|---|---|---|
| nylon | Even wear life (ISO 13934 tensile to spec); good abrasion resistance (ISO 12947 as specified); stable for branding | US$1.6–5.5 / meter (per the specification) | Volume styles with predictable yield | Advantages: versatile. Trade-offs: performance depends on coating/finish | Lock coating spec, color tolerance and print compatibility; confirm reinforcement mapping |
| PU coated polyester (600D, per spec) | Good repellency (ISO 4920 / AATCC 22 per the specification); moderate barrier (ISO 811 as specified) | US$1.2–6.0 / meter (to spec) | Value/core lines where print clarity matters | Advantages: cost controlled. Limitations: coating wear over time | Define spray rating targets and abrasion benchmarks; protect high-wear zones |
| Canvas / cotton (per the specification) | Good hand-feel and print; waterproofing depends on finish (AATCC 22 to spec) | US$1.0–3.5 / meter (to spec) | Retail lifestyle lines, totes and promotions | Upsides: classic look. Limitations: heavier; stain risk without finish | Define shrinkage and colorfastness tests (AATCC 61 / ISO 105 per the specification); specify lamination if needed |
Screening fabric options without a lab
- Read the scenario first, then let wear points and wet exposure narrow the options.
- Main compartment only is one option; decide if the claim spans the whole bag or zones.
- Cite the ISO, AATCC or ASTM references in your pack and state what passes.
- Pick trims that suit the chosen route: zipper type, sliders, buckles and webbing strength.
- Print and branding compatibility is confirmed on the real fabric.
- Evaluate transit rubbing risk, because visible creases are freight damage far more often than stitching faults.
Specifying the Product Before Tooling Starts
What makes a pack quotable in 24-48 hours
Order of operations for an OEM or ODM build
- Nail the user, the band and the proposition before anything else.
- Lock claim scope, then confirm the test plan to spec.
- To build it, add the BOM, then the measurement table, then the tolerance map, then artwork placement.
- Prototype sampling validates fit, structure and the material route.
- By PP, BOM and packaging route are final.
- First, sign the QC checklists and golden sample; only then cut bulk.
Before you approve: the sample checklist
- Confirm fabric shade and coating feel with the actual supplier lot (to spec).
- Testing to spec means stressing the webbing, the handles and each D-ring junction.
- Run the open/close and pack cycle many times: corner wear and seam creep are what to watch.
- Test method pack resistance to abrasion resistance, folding, and dampness before trusting it on the lane.
- A final BOM and a final packing route go into the PP sample awaiting approval.
- Changes stop at freezing, so bulk cutting runs without late feature creep.
How to reach a signed sample faster
What a repeat order should look like
Success example (anonymized): a mid-range program targeting United States reduced rework by freezing a single tech pack, running one pre-production sample using the final BOM, and aligning QC checkpoints before cutting. Reproducible builds remove the annual need to qualify someone new when reordering.
Production & Manufacturing Methods for Duffel Bags
Ordering choices get clearer once you compare lead time, MOQ requirements and cost bands in the table.
Specifying the construction route
Decoration and Assembly Controls
Marking methods, ranked by durability
Final-stage controls worth enforcing
From Port to Warehouse
Documents and timing gates
Key Factors to Choose a Reliable Duffel Bags Manufacturer
Use this checklist before signing an OEM/ODM contract for duffel bags.
Screening questions that separate routes
- Is the quote traceable to your spec, with assumptions listed?
- Can they source the BOM and also suggest alternatives that meet spec?
- Is there an AQL plan, and do QC checkpoints cover IQC through IPQC into FQC?
- Can workmanship survive a flexible MOQ arrangement?
- Can you expect firm lead times and a clear escalation procedure?
- Does their track record include packaging and shipping into your market?
Questions to put to the production team on site
Relative advantages at a glance
Developing the body, end panels and zipper path
A duffel is drafted as a body panel plus two end panels, not as a single continuous wrap. The wrap approach looks cheaper on a marker but it forces the zipper to travel around two corners, and that is where the bowing and zipper fatigue complaints originate. QUANZHOU JUNYUAN BAGS separates the panels so each element can be dimensioned independently.
The main opening is drafted as a straight run wherever the silhouette allows it. Where a horseshoe opening is required for access, the curve radius is held generous enough that the tape is not forced to compress on the inside of the turn, and the pattern includes a facing that stabilises the tape bed rather than relying on the shell alone.
Ease is built in deliberately. A 40 litre duffel is not a 40 litre box; the pattern carries enough ease at the end panels that the bag reads as soft-sided and can be compressed for freight without the shell puckering at the seam lines.
Handle anchorage, base and load path
Handles are the highest-load point on any duffel and the pattern has to reflect that. The webbing is drafted to run under the body panel and terminate in a boxed-X stitch field rather than stopping at the seam, so the load path runs into the shell instead of into a single line of stitching. A wrapped handle pad is patterned separately and dimensioned against the webbing width.
| Pattern element | Typical specification | Failure it prevents |
|---|---|---|
| Handle webbing | Runs under body panel, boxed-X stitch field | Strap pull-out at the seam |
| Base panel | Separate piece, coated or double-layer | Sagging and abrasion wear-through |
| Zipper path | Straight run, faced tape bed | Bowing and slider fatigue |
| End panels | Drafted with ease for compression | Puckering along the seam line |
The base is patterned as its own piece in a coated or double-layer material, sized so it sits slightly proud of the body. That keeps abrasion off the shell seam and gives the bag a flat footprint when set down loaded. Corner gussets are kept shallow so the footprint does not balloon.
A removable shoulder strap adds a second load path, and the D-ring anchorage is patterned with its own reinforcement so the two systems do not share a single stress point. Sampling for a duffel runs 6 to 10 working days, extending to 12 to 15 working days where a moulded handle or branded puller is specified.
Zipper selection is part of the pattern decision, not a separate one. A number 8 coil gives a smooth run on a long opening, while a number 10 moulded chain reads more robust and suits a heavier shell. The tape bed width in the pattern has to suit the chosen chain, so the two are specified together in the tech pack.
Interior organisation is drafted after the load path, not before. Slip pockets and a lined end pocket are added once handle and strap anchorage are settled, because reinforcement patches behind those anchorages change what interior space is actually available.
Pattern work is quoted with tooling shown separately; QUANZHOU JUNYUAN BAGS responds within 24 to 48 hours. Construction sequencing is set out in bag manufacturing process, and strap options are compared under custom travel bags.
Size ladder: capacity, fabric consumption and carton volume
A duffel range is usually sold as a ladder of two or three capacities, and the pattern work is mostly about how that ladder is built. Grading a 40 L pattern up to 60 L is not the same as drafting a 60 L shell: panel curvature, base board thickness and handle anchorage all change. The table below gives the planning numbers used before a size set is quoted.
| Capacity | Dimensions (cm) | Shell fabric, linear m at 150 cm | Flat-pack CBM per 10 |
|---|---|---|---|
| 30 L | 48 x 26 x 26 | 1.85 | 0.052 |
| 40 L | 55 x 28 x 28 | 2.25 | 0.068 |
| 60 L | 65 x 32 x 32 | 2.95 | 0.098 |
| 90 L | 75 x 36 x 36 | 3.70 | 0.135 |
Two decisions follow from these numbers. First, whether each size is its own SKU or a size variant, because MOQ 500 applies per colourway and a three-size ladder can mean 1,500 units rather than 500. Second, how the order ships: 500 flat-packed 40 L duffels occupy about 3.4 CBM, so a 20GP at 28 CBM carries the ladder comfortably and leaves room for a mixed carton run.
Pattern details that fail on the line, and the fix for each
The pattern is where a duffel either sews cleanly at speed or fights the operator on every unit. These five details account for most of the rework seen on new duffel introductions.
- Zipper path longer than 60 cm bows at the centre: specify the tape 3 mm short of the finished opening and add a 10 mm boxing at each end to absorb the tension.
- Handle root pull-out on a loaded bag: bar-tack 12 mm x 25 mm across the webbing and extend the reinforcement patch 40 mm past the stitch line into the body panel.
- Base sag on a 60 L or larger shell: add a 1.2 mm PE board and build 5 mm of ease into the base panel so the fabric is not carrying the load on its own.
- Fraying at bound internal seams: 10 mm seam allowance with 20 mm binding, sewn single-needle at 8–9 stitches per inch, and no raw edge left inside the binding.
- Revision control: budget two rounds at 6–10 working days each; a third round means the tech pack is missing tolerances, not that the pattern is wrong.
Every one of these is cheaper to fix on the pattern table than on the line, and all of them cost nothing to specify correctly in the first place. Our production team marks all five on the first pattern sheet so the sample round catches them rather than the bulk run. See the manufacturing process for how the approved pattern moves into cutting and assembly.
Frequently Asked Questions (FAQs)
Why should a duffel use separate end panels rather than one continuous wrap?
A forced wrap makes the zipper travel around two corners, which is where bowing and slider fatigue start. Separate end panels let the opening run straight and let each element be dimensioned independently, so the tape bed stays flat through the full length.
How is the main zipper path drafted to avoid bowing on a long opening?
The path is kept straight wherever the silhouette allows, and where a curve is unavoidable the radius is held generous. A facing stabilises the tape bed rather than the shell alone, so the tape is not forced to compress on the inside of the turn.
What handle detail prevents strap pull-out on a loaded duffel?
Webbing is drafted to run under the body panel and terminate in a boxed-X stitch field instead of stopping at the seam. That moves the load path into the shell. A wrapped handle pad is patterned separately and dimensioned against the webbing width.
How is the base panel patterned so a loaded duffel does not sag?
The base is its own piece in coated or double-layer material, sized slightly proud of the body so abrasion stays off the shell seam. Corner gussets are kept shallow, which stops the footprint ballooning when the bag is set down loaded.
How much ease should be built into a 40 litre duffel pattern?
Enough that the bag reads as soft-sided and compresses for freight without the shell puckering at the seam. Ease is carried at the end panels rather than in the body, so the printed front face stays flat and the panels still stack cleanly.
Does adding a removable shoulder strap change the duffel pattern set?
It adds a second load path. D-ring anchorage is patterned with its own reinforcement so the handle and strap systems do not share one stress point. The strap pad and slider detail are dimensioned against the webbing width in the same tech pack.
When does a duffel need a new pattern rather than a size variant?
A size variant works when only body length and end panel scale change. A new pattern is needed if the opening geometry, base construction or handle load path changes, because those alter the load distribution rather than just the volume.
How long does duffel sampling take when a moulded handle is specified?
Standard sampling runs 6 to 10 working days. A moulded handle or branded zipper puller extends it to 12 to 15 working days because tooling has to be cut first. Bulk production then runs 35 to 50 days after pre-production approval.
Continue Reading
Internal resources
Related blog posts
- The Hidden Costs of Custom Bag OEM (And How to Reduce Them)
- The Ultimate Guide to Waterproof Dry Bags for Outdoor Brands
- Tool Bag Hardware: Metal Buckles & Plastic Base Feet
- Tool Bag Production: Quality Control for Heavy Use
- Submersible Waterproof Bags: Engineering & Testing
- Tactical Backpack Manufacturing: MOLLE Webbing & Durability
Next step
• Lock keyword and claim scope for custom duffel bag oem
• Build a tech pack with BOM + tolerance map
• Choose materials route and validate tests (by spec)
• Plan sampling gates (lead time 6-10 working days)
• Set MOQ and cost targets (MOQ 500 pcs)
• Define QC plan and AQL checkpoints
• Confirm production + shipping timeline (35-50 days)

Get a quote for your next build
Your requirements go in; a structured RFQ checklist and manufacturing plan come out.
Related programme guides: custom travel bags.
End panels, zip paths and where duffel patterns go wrong
A barrel duffel is a cylinder closed by a zip that has to travel around two corners without going tight or wavy. Almost every duffel pattern problem traces back to one of three relationships: the end panel circumference versus the body panel length, the zip path versus the grain line, and the haul-handle anchoring versus the load it actually sees when the bag is lifted one-handed off a conveyor.
Circumference mismatch is the classic. The end panel is an ellipse or a rounded rectangle, and its perimeter must equal the body panel width plus two seam allowances, within a tolerance of about 3 mm. Too long and the end panel puckers in a ring of small pleats that no amount of pressing removes; too short and the body panel is pulled flat across the ends, the bag loses its cross-section, and the internal volume drops by 10 to 15% against the design intent. The fix is arithmetic done before the marker is cut, then confirmed on a toile, not on the first sewn sample.
Zip path is the second. A zip that runs the length of the body and turns down the end panels should follow the seam line, with the zip tape eased around the curve at no more than 4 mm of ease per 100 mm of radius. Where a design wants the zip to cut diagonally across the end panel instead, the tape is no longer on the straight grain and it will lengthen under load, producing the familiar wave along the closed zip. Either accept the wave as a design feature and stabilise the tape with a fusible strip, or move the zip back to the seam. Diagonal zips also complicate the marker, and marker efficiency is a direct cost input.
| Size | End panel | Zip length | Marker yield | Indicative FOB Xiamen |
|---|---|---|---|---|
| 30 L, 450 mm | Ellipse 260 x 220 mm | 520 mm | 88 to 92% | 4.50 to 6.00 |
| 45 L, 550 mm | Ellipse 320 x 260 mm | 640 mm | 84 to 88% | 5.50 to 7.50 |
| 60 L, 620 mm | Rounded rect 360 x 300 mm | 760 mm | 80 to 85% | 6.50 to 9.00 |
| 90 L, 750 mm | Rounded rect 420 x 360 mm | 900 mm | 74 to 80% | 8.00 to 12.00 |
Anchor points, marker yield and the cost of changing your mind
Handles on a duffel are loaded in a way backpack straps never are: the bag is grabbed and swung, so a 20 kg duffel can put a shock load well above 60 kg through a single handle end. The pattern answer is a continuous webbing loop that runs under the body panel rather than two separate tabs stitched onto the surface, plus a reinforcement patch that extends past the bar tack by 20 mm on every side. A surface-tabbed handle will pass a static pull test and still fail in service, because the failure is peel at the tab edge rather than tension through the webbing.
Then there is yield. On a 600D body at 150 cm usable width, marker efficiency typically lands between 74 and 92% depending on how awkward the panel shapes are, and every lost percentage point is fabric you paid for and cannot sell. That is why a duffel that shares its panel geometry with an existing size band is cheaper per unit than a bespoke silhouette even when the bill of materials is identical. It is also why a pattern change after sampling carries real cost: new cutting dies or laser files sit in the USD 300 to 2,500 tooling band, and the 35 to 50 day mass production clock restarts from sample approval.
Plan the pattern approval as a gate, not a conversation. Freeze circumference, zip path, handle anchoring and reinforcement patch geometry on the pre-production sample, and treat anything after that as a change order. Volumes start at 500 units per style and colour, repeat programmes can discuss 300, and quotes are returned in 24 to 48 hours. Construction detail and its cost consequences are covered further in the cost and MOQ guide, while the wider build sequence sits in the manufacturing process overview. If the brief leans toward a shorter, squarer silhouette with a shoe compartment, the gym bag pattern notes are the closer comparison.
Numbers age badly when copied into dozens of places, so the maintained version of this grid stays on quality control and certification.
Rather than repeat the same matrix here, keep the detailed grading with the central reference on material selection — it lists the acceptance numbers and sampling levels our team works to.