Your Trusted Custom Waterproof Pouches Manufacturer
Compact waterproof pouches for phones, documents, and valuables. OEM/ODM customization with sealed construction and reliable closure systems for outdoor and travel brands.
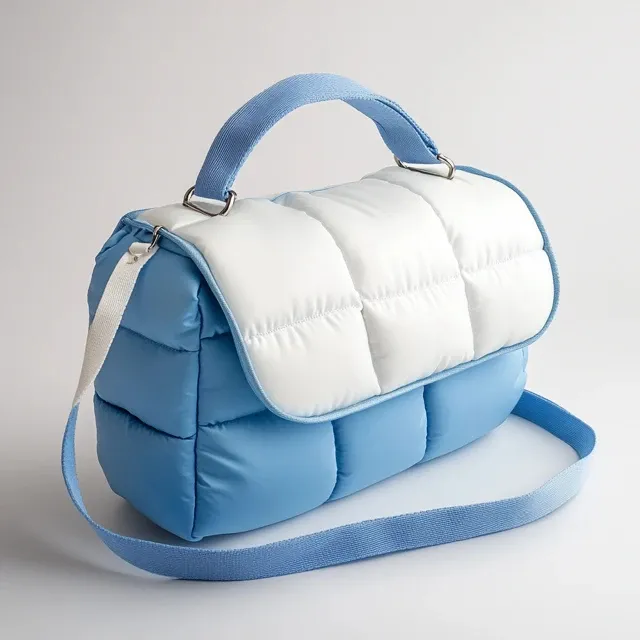
Spec snapshot
A fast engineering view of what matters for sourcing, quoting, and repeatable production.
| Item | Typical | Notes |
|---|---|---|
| Use scenario | beach / boating / rafting / travel | Scenario defines waterproof target and strap/hardware needs |
| Seal type | ziplock + lock / clamp / zipper (by spec) | Seal usability drives real-world performance |
| Window choice | TPU window / no-window | Window affects usability and seam leakage risk |
| Attachment system | neck strap / waist belt / float option (by spec) | Attachment points must be reinforced for repeated pulls |
| Typical MOQ | 500–2000 pcs | Depends on custom molds, printing, and accessory sets |
Device fit & usability
Waterproof pouches are bought for fit and usability. Define your target devices and we will engineer window, seams, and closure accordingly.
| Device / item | Max size | Fit notes |
|---|---|---|
| Phone pouch (standard) | up to ~6.7" phones | Define phone + case thickness; window size changes seam layout |
| Phone pouch (large) | oversize phones + thick case | Recommend larger gusset and lanyard reinforcement |
| Passport / documents | passport + folded papers | Prefer wider opening for fast access and reduced seal stress |
| Key / small gear pouch | keys, cards, small accessories | Smaller pouches benefit from simplified seal geometry |
Seal system trade-offs
Most “waterproof” issues come from seal usability: how customers close it, reopen it, and how the seal ages. Choose the right system for your claims.
| Seal type | Pros | Cons | Best for |
|---|---|---|---|
| Double ziplock + slide lock | low cost, lightweight, easy packaging | relies on correct closure by user; seal ages over time | entry-level pouches and travel accessories |
| Clamp-style seal | clear user feedback on closure; stronger mechanical lock | higher part cost; clamp fit tolerance control needed | outdoor and higher-claim programs |
| Waterproof zipper (by spec) | fast access and premium look | zipper ends are leak risk; higher cost and assembly complexity | premium pouches requiring frequent access |
| Roll-top mini pouch (by spec) | robust waterproofing when closed correctly | slower access; not ideal for phone touchscreen use | small gear and boating accessories |
Waterproof rating options (IPX)
We can engineer materials, seams, and closures to match different waterproof performance targets.
| Level | Meaning | Factory notes |
|---|---|---|
| IPX6 | Heavy splashing / water jets | For beach and boat splash protection; seal usability matters. |
| IPX7 | Temporary immersion | Requires stricter seal system and validation plan by spec. |
Materials & fabrics
Material choice drives performance, durability, finishing, and target price point.
| Fabric | Waterproof | Cost | Notes |
|---|---|---|---|
| TPU film laminate | IPX6–IPX8 (by design) | varies | Clear windows and sealed edges for pouch applications. |
| PVC film | IPX6–IPX7 (typical) | varies | Cost-effective for mass programs; pairing with sealing process is key. |
| Coated nylon (TPU/PVC) | water-resistant to waterproof | varies | For soft pouch styles and branding options. |
• Roll-top or waterproof zipper options
• Lanyard / neck strap / waist strap add-ons
• Clear window, ID slot, and reflective trims
• zipper/closure function test
• immersion test by sampling plan
• strap pull test for attachment points
• Kayaking & SUP: splash and immersion protection
• Travel: passports and documents protection
• Outdoor events: valuables storage for participants


• Seal type preference and closure usability expectation
• Device list and max size (phone model + case thickness)
• Window requirement (touchscreen use vs no-window)
• Attachment system (neck strap, belt, float option) and load expectation
• Branding method and packaging requirements (retail kits vs bulk)
Start custom waterproof pouches production
Send your requirements and get a structured RFQ checklist and a manufacturing plan.
Specification options for sealed soft pouches
A sealed pouch looks like the simplest product in a range and is one of the easiest to get wrong, because performance concentrates in two places: the film and the join. The brief should open with what goes inside, how long the unit stays submerged or exposed, and whether it sells on a retail card or packs inside a larger product.
| Specification | Standard range | Development notes |
|---|---|---|
| Flat dimensions | 12 × 18 cm to 30 × 40 cm | Largest item plus a 10–15 mm handling margin |
| Film and laminate | TPU 0.15–0.40 mm, PVC 0.30–0.50 mm, EVA shell 2–5 mm | TPU holds flexibility in cold; PVC is the cost floor |
| Join method | High-frequency weld 6–12 mm wide, or hot-air seam tape | Weld width drives peel strength and edge appearance |
| Peel strength | 25–45 N per 25 mm | Measured on production parts, not lab coupons |
| Closure | Roll-top with 3–4 folds, waterproof coil zip #5 or #8 | Roll-tops tolerate abuse; zips win on access speed |
| Ingress performance | IPX6 splash resistance to IPX8 immersion, 1 m for 30 minutes | Rating must match the claimed use case |
| Service temperature | -20 °C to 60 °C | Cold bend behaviour separates TPU from PVC |
| Compliance lines | FDA 21 CFR film, REACH (EC 1907/2006), EN 71-3, California Proposition 65 | Children's and food-adjacent SKUs widen scope |
Film choice decides most programmes. PVC is the cost floor and prints well, but it stiffens noticeably in cold conditions and carries a heavier compliance conversation in several markets. TPU costs more per metre, welds at different energy settings and holds flexibility down to freezing. Where the pouch must hold shape rather than only exclude water, a moulded EVA shell beats a thicker film.
Join geometry deserves as much attention as the film. A 6 mm weld looks tidier than a 12 mm weld, but peel strength rises with width and narrow welds curl sooner, so visual preference and mechanical requirement have to be reconciled before tooling is cut. Corner radius is the other quiet variable. Material behaviour is summarised under film, coating and laminate selection.
How sealed soft pouches are built
Production begins with a nesting plan rather than a cutting list. Film arrives in rolls with a grain direction, and welds behave differently with and across it, so panel geometry keeps the critical joins running predictably. Die-cutting is used where volumes justify the tooling; below that, a guided knife or laser cut is used and the edge is finished in the weld.
High-frequency welding is the default join for thermoplastic films. Electrodes are machined to the panel profile and the variables that matter are energy, dwell time and pressure. Under-welded joins pass a visual check and then peel apart in the field; over-welded joins thin the film at the weld boundary and fail at the edge instead. Settings are recorded per material lot.
Hybrid builds combine film with a textile face: the fabric panel joins the film with hot-air tape or a welded transition strip, and any stitch line is kept away from the water path. That is how a soft outer or a printed brand panel gets added without perforating the waterproof layer.
Closures are fitted as a sub-assembly. Roll-tops are the most forgiving option: three folds give splash resistance, four give immersion performance, and there is no mechanical part to fail. Waterproof coil zips open faster and read as premium but bring their own tolerance stack. Our 4,950 m² SGS-verified production floor carries dedicated welding cells, with 137 people trained on both welding and inspection.
Cost drivers and MOQ for sealed soft pouches
Film is the largest material line, and gauge is the lever buyers underestimate. Moving from 0.25 mm to 0.40 mm TPU can add a fifth to material cost without feeling any better, while the same money on a moulded shell or a better closure changes perceived quality immediately. After film comes the closure, then tooling for dies and electrodes.
Printing is the second cluster. Film surfaces accept screen and UV print well but usually need a primer or corona treatment, and multi-colour artwork on a small part carries a setup cost that behaves like tooling. For several colourways, print one film lot and differentiate by trim, which keeps every colour on a single film minimum.
| Construction | Typical build | Indicative unit price (USD) |
|---|---|---|
| Flat welded sleeve | 0.25 mm film, roll-top, single-colour print | 1.20–2.40 |
| Zipped flat pouch | Waterproof coil zip #5, welded seams | 2.40–4.20 |
| Moulded shell pouch | 3–5 mm EVA shell, textile liner, welded joins | 4.20–7.50 |
| Retail-ready assembly | Strap or lanyard, hang card, barcode, polybag | 7.00–12.00 |
Minimums begin at 500 units per style per colour, reducing to 300 on repeat programmes once electrodes and dies exist. Sampling runs 6–10 working days, extending to 12–15 where a moulded shell or custom closure is commissioned, and mass production takes 35–50 days after written approval. Terms are T/T 30/70, quotations are returned in 24–48 hours, and dispatch is FOB Xiamen with EXW, CIF or DDP available. Tooling sits at USD 300–2,500, and the USD 50–150 sample fee is credited to your first bulk order.
These parts are light but bulky once packed, so carton efficiency usually decides whether landed cost is profitable or marginal. Plan against 28 CBM per 20GP, 56 CBM per 40GP and 68 CBM per 40HQ, and choose sea at 25–35 days unless a launch date forces air at 5–8 days; courier at 3–5 days covers samples. How quantity reshapes tooling amortisation is explained in our cost and quantity planning reference.
Quality gates and acceptance criteria
Weld integrity is tested on production parts, not coupons. Peel strength is measured to ASTM D751 on coated and film materials with 25–45 N per 25 mm as the working band, and the failure mode matters as much as the number: peeling at the weld boundary indicates over-welding, peeling inside the weld indicates insufficient energy or contamination.
Ingress is verified two ways. Film resistance is measured as hydrostatic head under AATCC 127, and assembled pouches are exposed in a spray cabinet under AATCC 22 or a shower cycle under AATCC 35 with a paper load inside. Immersion claims are tested to the marketed rating rather than inferred from a splash result.
Chemical compliance is scoped by destination and end use: food-adjacent pouches use film documented under FDA 21 CFR, children's lines are screened to EN 71-3 and CPSIA, printed areas against California Proposition 65, and all inputs against REACH (EC 1907/2006). Finished goods are inspected to AQL 2.5 under ISO 2859-1 with Critical 0, Major 2.5 and Minor 4.0, AQL 1.5 where tighter control is needed, and prints are checked for transfer under AATCC 8.
Closure systems, ingress ratings and retail presentation
An ingress rating is a claim, and claims need evidence. A pouch sold for use inside a larger bag does not need an immersion rating, and specifying one raises cost without changing the customer experience. Anything marketed for paddling or water sports needs a tested figure, and the rating on the packaging has to match the rating in the report.
Retail presentation changes the build more than most briefs allow for. A hang card needs a reinforced hole or a welded loop, shelf presentation favours a moulded shell that stands up, and e-commerce favours a flat pack that photographs cleanly. Carry closure and trim language across the family so it reads as one programme; our private label programme page covers how that is standardised. Small parts also pair well with coordinated soft pouches for cosmetics and accessories.
Ordering path
Six stages from contents brief to packed cartons.