Your Trusted Custom Handbags Manufacturer
Handbag manufacturing for fashion brands, from structured PU leather handbags to lightweight nylon daily bags. Focused on shape, finishing, and hardware quality.
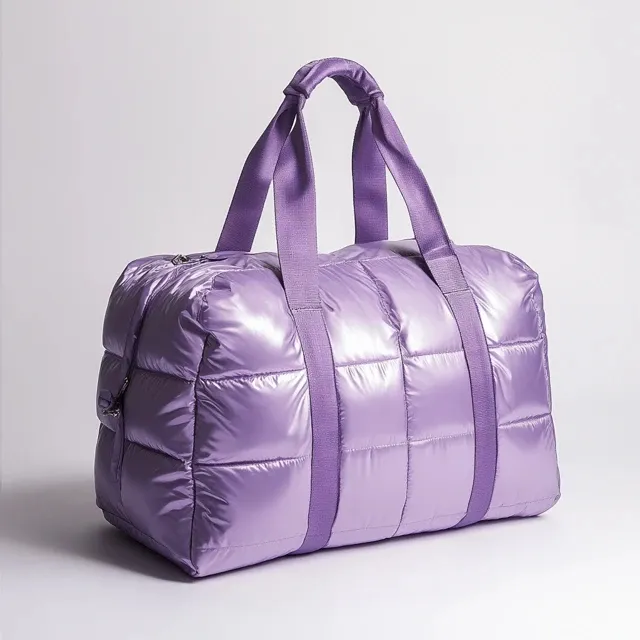
Spec snapshot
A fast engineering view of what matters for sourcing, quoting, and repeatable production.
| Item | Typical | Notes |
|---|---|---|
| Structure level | soft / semi-structured / structured | Structure defines silhouette, feel, and cost |
| Edge finishing | edge paint / binding / turned edge | Finishing is where premium shows up |
| Hardware tone | gold / nickel / gunmetal (by spec) | Define finish tolerance and scratch expectations |
| Typical MOQ | 500–1,000 pcs | Depends on materials, hardware, and packaging |
Structure & silhouette engineering
Handbags are sold by silhouette. Structure is an engineering choice: reinforcement, lining, and edge finishing determine how the bag holds shape over time.
| Module | Options | Why it matters | Notes |
|---|---|---|---|
| Reinforcement panels | structured boards / foam / no board (by spec) | controls shape and standing silhouette | Define crease points and fold behavior |
| Base construction | reinforced base + feet (by spec) | prevents sagging and early wear | Base wear is a common complaint in daily use |
| Handle anchors | wrap anchors + reinforcement patches | handle failures create returns | Align reinforcement to load target and carry style |
| Lining strategy | full lining / partial / premium lining (by spec) | affects perceived quality and durability | Avoid lining wrinkles and pocket distortion |
Edge finishing playbook
Edge finishing is where “premium” shows up. Choose a method that matches material, channel, and wear expectations.
| Method | Best for | Limitations | QC focus |
|---|---|---|---|
| Edge paint | PU/leather premium lines | requires process control for cracking resistance | paint thickness uniformity + adhesion checks |
| Binding | nylon/canvas styles and sports-fashion | visible seam line; depends on binding quality | binding tension and stitch alignment checks |
| Turned edge (by spec) | premium minimalist silhouettes | adds labor and material allowance | edge thickness consistency and corner execution |
Hardware plating consistency
Retail handbag perception depends on consistent hardware color, gloss, and scratch tolerance. This section defines finish controls and inspection points.
| Hardware | Finish | Risk | QC checks |
|---|---|---|---|
| Buckles and rings | plating tone by spec | tone mismatch across batches | finish sampling + color tolerance control |
| Logo plates (by spec) | plating + scratch tolerance | micro-scratches and gloss inconsistency | scratch inspection and protective film control |
| Zipper pullers | matching tone | inconsistent feel and appearance | zipper run checks + finish inspection |
Materials & fabrics
Material choice drives performance, durability, finishing, and target price point.
| Fabric | Waterproof | Cost | Notes |
|---|---|---|---|
| PU leather | depends on finish | varies | Stable appearance and easy maintenance. |
| Genuine leather (by program) | depends on finish | varies | Premium hand-feel for high-end lines. |
| Nylon | water-resistant options | varies | Lightweight everyday handbags. |
• edge painting or binding (by spec)
• lining pocket layout
• hardware plating consistency
• hardware plating checks (by spec)
• AQL final inspection
• Boutique collections
• Private label handbags
• Material choice (PU/leather/nylon) and structure level
• Edge finishing preference (paint/binding/turned edge)
• Hardware tone and finish tolerance requirements
• Pocket layout and lining preference
• Packaging requirements (dust bag, tissue, box, inserts)
Start custom handbags production
Send your requirements and get a structured RFQ checklist and a manufacturing plan.
A handbag has to look right while it is empty. That one requirement drives nearly every decision behind a leather or PU handbag programme: the body must stand on a shelf with nothing inside it, keep its line after a week of daily use, and still feel light on the shoulder once it is full. Programmes that start from the outside silhouette and work backwards usually sample three times. Programmes that settle interlining, handle load paths and edge finish on paper first normally approve on the first or second round.
Specification options for custom handbags
The grid below is the reference our production team prices against once a drawing, a tech pack or a reference sample arrives. Read the structure row before the material row — interlining choice decides whether a soft top-grain shell slumps or holds, and it is the line most buyers revise after seeing the first sample of custom handbags.
| Parameter | Top-handle 22 cm | Shoulder 30 cm | Tote 36 cm |
|---|---|---|---|
| Capacity | 4 L | 8 L | 14 L |
| External dimensions | 22 × 18 × 10 cm | 30 × 24 × 12 cm | 36 × 30 × 14 cm |
| External dimensions tolerance | ±2 mm | ±2 mm | ±3 mm |
| Shell material | Full-grain cow, 1.2 mm | Top-grain cow, 1.0–1.2 mm | PU-coated split, 0.9 mm, or 900D PU |
| Lining | 210D polyester twill, 1 slip pocket | 420D polyester, 2 slip + 1 zip pocket | 420D RPET, 3 pockets, key clip |
| Structure | 0.6 mm non-woven + 1.0 mm EVA sheet | 0.8 mm foam laminated to shell | 1.2 mm EVA base board, foam walls |
| Closure | Metal frame with kiss-lock | Magnetic snap on reinforced tab | Open top, magnetic tab + inner zip |
| Handle | Rolled leather, 10 cm drop | Flat leather, 25 cm drop | Full-wrap webbing core, 26 cm drop |
| Strap | Detachable chain, 55 cm | Adjustable, 110–125 cm | Removable webbing, 60 cm |
| Hardware finish | Light gold, nickel-free plating | Gunmetal, EN 1811 compliant | Brushed antique brass |
| Base | 4 metal feet, riveted with washers | 4 feet, reinforced base panel | 5 feet, 1.5 mm board |
| Empty weight | 420 g | 640 g | 880 g |
| Colourways per drop | 2–3 | 3–4 | 4–6 |
How custom handbags are built
Pattern work starts from the finished silhouette, not from a flat drawing. A 30 cm shoulder bag normally breaks into five panels — front, back, two gussets and a base — and the gusset width is what sets how much the bag can hold before the front face bulges. We hold panel tolerance at ±2 mm because a 3 mm error on a gusset becomes a visible twist by the time the lining goes in.
Structure is the next decision. A soft top-grain shell laminated to 0.8 mm foam behaves completely differently from the same shell built over a loose 1.2 mm EVA board: the laminated version is lighter and packs flatter for shipping, while the board version holds a crisp edge and survives retail handling better. Base boards are non-negotiable above roughly 8 L; without one, contents load the bottom seam directly and the bag sags within weeks.
The handle is the part that fails first, so its load path is engineered rather than decorative. Rolled handles hide a webbing or cord core; flat handles hide a reinforcement plate sandwiched between shell and lining. Every D-ring is anchored to a webbing loop bar-tacked into the main seam, not stitched to the face, and rivets are set with backing washers so they cannot pull through under load.
Assembly runs either bag-in-bag or turned-through. Bag-in-bag gives cleaner internal seams and lets us finish the lining separately, which matters when you want a structured bag with a zip pocket stack; turned-through hides the top seam but limits how much pocketing can go inside. Edge finish closes the loop: three coats of edge paint with intermediate sanding on painted edges, or burnishing with gum tragacanth on vegetable-tanned leather. Stitch pitch sits at 7–8 stitches per inch, and the final operation is a shape check on the stand before packing.
Cost drivers and MOQ for custom handbags
Leather is the largest single line. Grade, thickness and cutting yield move together: full-grain from the prime area of the hide gives the best surface and the highest yield loss, while split keeps the metre price low but needs heavier PU coating to look even. Each colourway also carries a tannery dye-lot minimum, which is why the colour count in your drop matters as much as the unit count.
Labour minutes are the second driver, and handbags are handwork-heavy. Edge painting, handle wrapping, hardware setting and pocket building are all bench operations, so every extra pocket, every extra metal component and every extra stitch run adds minutes that no material saving offsets. Hardware specification is the third: nickel-free plating and branded pulls cost more than generic zamak, and custom dies are quoted separately.
Commercial terms are fixed and published: minimum order quantity is 500 units per style per colour, dropping to 300 for repeat programmes. Sampling takes 6–10 working days, or 12–15 for complex builds, and mass production runs 35–50 days after sample approval. Sample fees run USD 50–150 and are credited against your first bulk order; tooling such as emboss plates or custom hardware dies runs USD 300–2,500. Quotes come back in 24–48 hours, terms are T/T 30/70, and pricing is FOB Xiamen with EXW, CIF and DDP available. Our 4,950 m² SGS-verified production floor runs 7 lines with 149 machines and 137 people.
| Material tier | Indicative FOB band | Typical use |
|---|---|---|
| PU / bonded | USD 6.00–12.00 | Promotional and entry retail totes |
| Split leather, PU coated | USD 12.00–20.00 | Mid-market shoulder bags |
| Top-grain | USD 18.00–28.00 | Core retail programmes |
| Full-grain | USD 24.00–35.00 | Premium structured bags |
Quality gates and acceptance criteria
Inspection follows ISO 2859-1 at AQL 2.5 with Critical 0, Major 2.5 and Minor 4.0; AQL 1.5 is available on request for premium launches. On a handbag, a critical defect is a failed handle, broken hardware or a sharp edge; a major is a skipped stitch, cracked edge paint or panel misalignment beyond 2 mm; a minor is a light scratch or slight lining wrinkle that does not affect function.
Material compliance is tested per programme. Leather is checked to ISO 17075 for chromium VI, metal components to EN 1811 for nickel release, colour transfer to AATCC 8 dry and wet, seams to ISO 13934-1, and lining abrasion to ISO 12945. Destination rules are handled through REACH (EC 1907/2006), California Proposition 65 and CPSIA documentation as required.
Product-level tests close the loop: 500 handle lift cycles at 1.5 times rated load, a 25 kg static strap pull, 5,000 zip open-and-close cycles, a 0.8 m drop on the base with a 3 kg load, and a colour check under a D65 light box with a maximum deviation of 1.5 Delta E against the approved swatch. Anything failing at the gate goes back to the line rather than into the carton, and you receive the inspection report before balance payment.
Branding and packaging for handbag programmes
Branding on structured bags is usually applied before assembly, because a deboss or emboss needs flat access to the panel. Blind deboss, foil stamping, a stitched leather patch or a metal logo plate all work here; heat transfer and screen print suit PU shells and flat linings. Every personalisation step adds a station to the line and is costed per piece.
Retail packaging is quoted as its own line item: dust bag, tissue, care card, hangtag, barcode or GTIN label, and either a flat-packed or assembled carton. Carton specs are validated to ISTA 3A where the goods ship direct to a distribution centre. Volume planning is simple arithmetic: a 20GP holds roughly 28 CBM, a 40GP about 56 CBM and a 40HQ about 68 CBM, and handbags ship far better flat than stuffed.
Ordering path
Send a drawing or a reference sample and we will come back with an indicative FOB band, a sampling plan and a realistic production slot. See material options and cost and MOQ mechanics, or go straight to a quote request.