Your Trusted Custom Duffel Bags Manufacturer
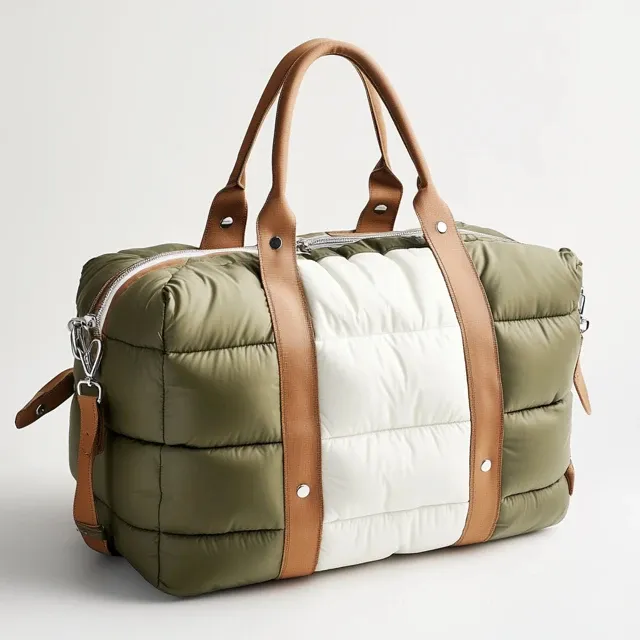
Duffel bag manufacturing for travel, gym, tactical, and retail collections. Designed for high stitch-load zones, clean finishing, and durable zipper and hardware execution.
Spec snapshot
A fast engineering view of what matters for sourcing, quoting, and repeatable production.
| Item | Typical | Notes |
|---|---|---|
| Carry mode | hand carry / shoulder / backpack straps (by spec) | Carry mode defines reinforcement and strap geometry |
| Typical size | 25L–45L / 50L–75L / 90L+ | Travel and gym programs often need multiple sizes in one line |
| Zipper strategy | #5/#8/#10 coil + end reinforcement | Zipper gauge and end structure are frequent failure points |
| Base durability | double layer / skid panel / molded base (by spec) | Bottom wear drives returns; define early |
| Pocket architecture | minimal / shoe compartment / wet pocket | Pocket complexity is a major assembly-time driver |
| Typical MOQ | 500–800 pcs | Depends on fabric dyeing, embroidery, and hardware customizations |
Cost drivers (what moves the unit price)
This makes quoting transparent and helps you choose performance upgrades that actually matter.
| Cost driver | Impact | How we optimize |
|---|---|---|
| Zipper length & gauge | Long main zippers and heavier gauges increase cost and assembly time | Choose gauge to match load; reinforce ends instead of over-spec everywhere |
| Pocket count & lining | Each pocket adds sewing operations and binding/lining cost | Use modular organization panels where possible |
| Carry system complexity | Backpack strap conversions add webbing/hardware and QA points | Design carry modes as clean modules with repeatable reinforcement |
| Base reinforcement | Skid panels and double layers add material cost but reduce returns | Target reinforcement only at high-wear zones |
| Branding package | Embroidery and molded patches affect lead time and MOQ | Prototype branding placements early to avoid rework |
Capacity & dimensions reference
Standard size options for duffel bags. We can also customize dimensions to fit your specific gear.
| Volume | Typical Dimensions | Best For |
|---|---|---|
| 25L - 35L | 50 x 26 x 26 cm | Gym and short trips |
| 40L - 55L | 60 x 30 x 30 cm | Weekend travel and carry-on style |
| 60L - 90L | 70 x 34 x 34 cm | Team gear and longer trips |
Materials & fabrics
Material choice drives performance, durability, finishing, and target price point.
| Fabric | Waterproof | Cost | Notes |
|---|---|---|---|
| 600D / 900D polyester | water-resistant options | varies | Cost-effective for gym and promotional programs. |
| 1680D ballistic nylon | water-resistant | varies | High abrasion resistance for travel and heavy use. |
| TPU coated fabric (by spec) | water-resistant to waterproof | varies | Easy cleaning and stronger protection. |
• zipper function cycle checks (by spec)
• drop test (by spec)
• AQL final inspection
• Gym and sports: high stitch-load durability and easy-clean liners.
• Tactical programs: abrasion materials and reinforcement at grab points.
• Corporate gifting: branded duffels with packaging alignment.

• Capacity target and size run (single size vs multi-size collection)
• Pocket architecture (shoe compartment, wet pocket, laptop sleeve by spec)
• Fabric preference and abrasion/water-resistance requirement
• Zipper gauge preference and any branded zipper pulls
• Branding method (patch/embroidery/print) and placement
• Packaging requirements and target delivery date
Start custom duffel bags production
Send your requirements and get a structured RFQ checklist and a manufacturing plan.
A duffel looks simple and is not. One very long zipper carries most of the structural load, the handles wrap under a body with no frame to support them, and the whole thing is expected to hold its shape when empty and survive being thrown when full. Three elements decide its life: the main closure specification, how the handle webbing is routed, and the base.
Specification options for custom duffel bags
The tiers below are dimensioned around real logistics rather than round numbers: a 60 L cabin-plus size that most travellers can legally carry, and sizes above it that cannot be sold as airline-friendly anywhere. Everything else in the grid is the set of decisions our production team needs before quoting.
| Parameter | Cabin 40 L | Weekend 60 L | Expedition 90 L |
|---|---|---|---|
| Capacity | 40 L | 60 L | 90 L |
| Overall dimensions | 50 × 28 × 26 cm | 60 × 32 × 30 cm | 72 × 38 × 34 cm |
| Shell fabric | 420D polyester, PU back | 600D recycled polyester, TPU back | 900D polyester with PVC reinforcements |
| Lining | 210D polyester, undyed | 210D dyed to match | 420D ripstop, dark grey |
| Main closure | #10 coil, straight run | #10 reversed coil, horseshoe path | #10 coarse with storm flap and dual slider |
| Base | Folded shell with 5 feet | EVA board in a sewn pocket, 5 feet | Moulded EVA tray with 8 feet and drain |
| Carry modes | Wrap handles plus webbing sling | Wrap handles plus padded removable sling | Wrap handles, removable padded harness, grab ends |
| Handle construction | 25 mm webbing, continuous under body | 38 mm webbing with neoprene grip | 38 mm webbing with moulded grip, box-stitched |
| End compartment | None | Ventilated shoe pocket to EU 46 | Shoe pocket plus wet compartment with welded liner |
| Empty weight | 780 g | 1,150 g | 1,780 g |
| Documented compliance | REACH (EC 1907/2006), Proposition 65 | REACH, CPSIA, amfori BSCI, OEKO-TEX Standard 100 | REACH, CPSIA, Sedex SMETA, OEKO-TEX Standard 100, ISTA 3A |
Watch the handle webbing specification carefully. A continuous run of webbing passing under the body is the only construction where the load is genuinely shared; two sewn-on hand loops rely entirely on stitch holding and will peel away at the same load that a continuous wrap shrugs off.
How a custom duffel is built
The main zipper is the structural spine. A straight zip along the top is easiest to sew and the most likely to fail under stress, because the corner where it turns takes the full opening force. A horseshoe path that continues down each end panel distributes that force and makes the opening usable, which is why most mid- and premium-tier duffels specify it.
That zipper should be reversed coil wherever appearance matters, because the coil then sits inside and only the tape shows. It also needs a bound rather than turned installation — the tape goes into a folded fabric channel that keeps dirt out of the teeth, with bar-tacks at both terminal ends where opening force concentrates.
Handles are routed as one continuous length of webbing running under the base, up both sides and over the top, joined at the summit. This is genuinely load-sharing rather than decorative, and it means load never travels through stitch holding alone. Where a neoprene grip is specified, we still run full webbing inside it so the grip is comfort rather than structure.
The base decision separates the tiers. Below roughly 45 L a folded shell with feet is adequate. Above that the bag needs an EVA board held in a sewn-in pocket so it can be replaced, and for anything above 80 L a moulded tray stops the bag collapsing into itself when set down half-packed.
End compartments introduce their own issues. A shoe pocket needs ventilation that does not admit water, meaning a mesh panel placed above the base line and a wipe-clean liner below it. A wet compartment should have welded seams, or a damp swimsuit will wick into the main cavity.
Finally, the strap option is where brand perception is decided. A webbing sling is cheap and adequate; a padded, removable strap with a swivel prevents the bag twisting on the shoulder.
Cost drivers and MOQ for duffel bags
Five things set price here, and the first surprises buyers: zipper length and grade. A 90 L duffel carries more than a metre of #10 chain, and upgrading from standard coil to reversed coil with a storm flap can add a meaningful percentage to unit cost. Then come base construction, strap assembly, fabric denier and packing method.
Programmes run from 500 units per style per colour, dropping to 300 on reorder once the markers and any tray tooling exist. Sampling is 6–10 working days on stock fabric and 12–15 where a moulded base or custom print strike-off is required, with tooling at USD 300–2,500 and sample fees of USD 50–150 credited against your first bulk order.
| Tier | Typical configuration | Indicative FOB |
|---|---|---|
| Entry | 420D shell, straight #10 zip, folded base, webbing sling | USD 5.80–8.50 |
| Mid | 600D recycled, horseshoe reversed coil, EVA board, shoe pocket | USD 8.50–12.50 |
| Premium | 900D shell, moulded tray, wet compartment, removable padded harness | USD 12.50–18.00 |
Terms are T/T 30/70 against FOB Xiamen, with EXW, CIF and DDP quoted under Incoterms 2020, and indicative pricing returned within 24–48 hours. Transit is 25–35 days sea, 5–8 days air and 3–5 days courier, and on duffels cube usually decides your order quantity before unit price does.
Quality gates and acceptance criteria
Inspection is AQL 2.5 with sampling per ISO 2859-1, Critical 0, Major 2.5, Minor 4.0, and AQL 1.5 available where your protocol requires a tighter window. Reports are issued from our 4,950 m² SGS-verified production floor, currently supporting about 200,000 units monthly across 7 lines.
The three predictive tests are the handle static load, the zipper endurance through its full curved path, and the carton drop test. Handle failure and zipper separation account for most duffel warranty claims in the field.
| Check | Method | Acceptance |
|---|---|---|
| Handle static load | In-house, 60 kg for 10 min | No stitch creep beyond 3 mm, no webbing slip |
| Loaded carry and drop | ISTA 3A, 10 drops at rated load | No functional damage, seams intact |
| Zipper endurance | In-house, 3,000 cycles full path | Smooth travel through corners, no separation |
| Seam strength | ISO 13934-1 | Above 200 N structural, above 150 N lining |
| Fabric tensile | ASTM D5034 | Above 500 N on shell fabric |
| Abrasion resistance | In-house Martindale, 30,000 rubs at base zones | No thread exposure or coating loss |
| Colour fastness to rubbing | AATCC 8 | Grade 4 dry, grade 3–4 wet |
| Hardware corrosion | ASTM B117, 48 h salt spray | No red rust on functional surfaces |
Cube, carton and freight planning for bulky duffels
Duffels are the classic case of a bag that quotes well and ships poorly. A 60 L unit occupies roughly 45–55 litres of packed volume even nested, and a 90 L unit ships air-filled unless it is rolled. Since a 20GP holds about 28 CBM, a 40GP about 56 CBM and a 40HQ about 68 CBM, the difference between nested, rolled and fully assembled packing can change your landed cost per unit more than a fabric downgrade would.
We include a carton-efficiency estimate with every bulk quote, so you see units per carton and per container before committing to a quantity. If you are building a full travel assortment rather than a single SKU, the custom travel bags page covers how mixed-SKU containers are optimised, and gym-club variants sit alongside them in the custom gym bags range.
Ordering path for duffel bag programmes
Six steps from brief to container, typically 10–13 weeks on a first programme where a moulded base or custom print is involved, and closer to 8–10 weeks on stock construction.
Send target capacity, carry preference and any airline constraint, and you will receive a build grid, a carton estimate and an indicative FOB band within 48 hours. Quantity economics are explained on cost and MOQ.