Waterproof Bag Packaging for Export & Retail
Discover how to run a custom waterproof bag oem program for North America: materials, tech pack, sampling, QC and shipping. Get OEM/ODM-ready checklists and


Inside the Build: How a Waterproof Bag Goes From Pack to Carton
Primary SEO focus: custom waterproof bag oem. Secondary: bag export logistics, waterproof bag manufacturer, private label bags, custom logo bags, OEM ODM bags.
Control points the build is measured against
Any tour worth taking is a control-point checklist in disguise, not a showroom trip.
Stage-by-stage: how the order is worked
- Brief alignment: settle the claim scope, cost target and packing rules before any sample.
- Within material sourcing, lock by spec: coating/laminate spec, fabric route, trim vendors.
- Pattern control: build templates, set a tolerance map, plan the reinforcement.
- Cutting stage: check grain direction plus marker efficiency; hold shade lots steady.
- Sewing and welding: hold the line on stitch spec, seam allowance, critical-zone reinforcement.
- At the final assembly stage, placement jigs position logos, hardware and accessories.
- Close with inspection: AQL sampling, carton marks and the export paperwork.
Typical buyer use scenarios
- outdoor sports
- fishing
- boating
- camping
- commuting
Key functions buyers request most
- RF welded seams
- roll-top closure
- airtight zipper option
- lash points
- abrasion reinforcement
Choosing the Best Materials for Custom Waterproof Bags
| Material | Performance | Cost Range | Leading For | Upsides & Trade-offs | Risks & How to Control |
|---|---|---|---|---|---|
| PVC tarpaulin (to spec) | Premium barrier and wipe-clean surface (ISO 811 / AATCC 127 as specified); strong scuff resistance tolerance (ISO 12947 as specified) | US$1.2–6.0 / meter (to spec) | Rugged utility lines and marine use | Upsides: durable surface. Watch-outs: heavier; sustainability concerns | Define fold/packout rules to avoid scuffs; control weight targets |
| Recycled RPET (route, to spec) | Sustainability positioning; performance depends on coating/laminate (ISO 4920 / ISO 811 per spec) | US$1.5–3.8 / meter (as specified) | Eco positioning programs and corporate procurement | Upsides: sustainability narrative. Watch-outs: supply stability and lot drift risks | Lock supplier lots, traceability and color delta; validate print and coating compatibility |
| Canvas / cotton (per spec) | Good hand-feel and print; waterproofing depends on finish (AATCC 22 as specified) | US$1.0–3.5 / meter (to spec) | Retail lifestyle lines, totes and promotions | Upsides: classic look. Trade-offs: heavier; stain risk without finish | Define shrinkage and colorfastness tests (AATCC 61 / ISO 105 per spec); specify lamination if needed |
Narrowing the material route quickly
- Work back from use: where it rubs, where it carries load, and how wet it gets set the route.
- Decide whether the claim covers the whole bag or only zones like the main compartment.
- Every referenced ISO/AATCC/ASTM procedure should be listed, together with the numeric bar for approval.
- Choose route-suitable trims, from zipper type and sliders to buckles and webbing strength.
- Confirm that print and branding suit the specified fabric.
- Scuffing and creasing usually trace to transit, not to stitching defects.
Design and Development: How the Build Is Specified
Tech pack contents that get a fast quote
Rather than restate a long matrix, this section points to custom backpack specifications, where each row carries its method and acceptance value.
The development sequence, as it really runs
- Pin down who buys it, at what retail band, and where it sits.
- Confirm the claim scope and its test plan by spec.
- Artwork placement, tolerance map, measurement table and BOM: four pieces that make the tech pack.
- Fit, structure and material route get validated at prototype sampling.
- Final BOM, final packaging route: the PP stage.
- Sign-off requirement: QC checklists plus the reference sample, ahead of bulk cutting.
Sample-stage checks that prevent expensive rework
- Verify artwork location physically on paper before the selected print process runs.
- Load-test every anchor point: webbing, grab handles and D-ring areas, to specification.
- Verify the zipper path, then slider feel, then the cycle requirement per spec.
- Open, close and repack the product many times, watching for corner wear and seam creep.
- Three things need checking per lane: rub marks, folding lines, and defence against humidity.
Fewer sample rounds: what actually helps
Why a repeatable build outperforms a hero sample
Production & Manufacturing Methods for Waterproof Bags
Weigh MOQ requirements against turnaround duration and price tier using the options table.
| Production Type | Lead Time | MOQ | Cost Level | Leading For |
|---|---|---|---|---|
| ODM catalog customization | 6-10 working days + 35-50 days | low–medium (to spec) | low–medium | Fast launches and proven silhouettes |
| Small-batch pilot run | 6-10 working days + 35-50 days | 500 pcs | medium | Startups, corporate gifting, SKU validation |
| Expedited production program | 15–25 days (per spec) | by program | higher | Time-critical launches |
| New tooling / new input materials route | sampling + production to spec | to spec | premium | New silhouettes and claim-led innovation |
Build methods worth naming in the pack
Branding and Final Assembly
Decoration routes available (pick one or two per SKU)
Closing-stage checks that cut return rates
Rather than repeat the same matrix here, keep the detailed grading with the central reference on material selection — it lists the acceptance numbers and sampling levels our team works to.
Freight, Documents and Delivery
Checkpoints on the shipping leg
Key Factors to Choose a Reliable Waterproof Bags Manufacturer
Use this checklist before signing an OEM/ODM contract for waterproof bags.
Partner selection checklist
- Will they price off your pack and show what they assumed?
- Are alternatives by spec offered, and BOM sourcing controlled by them?
- Do they evidence QC checkpoints, IQC to IPQC to FQC, and an AQL plan?
- Without hurting workmanship, can they allow a flexible MOQ?
- Can they give firm lead time commitments and a defined escalation path?
- Do they bring packaging and shipping know-how that fits your market?
What to verify when you walk the production site
Rather than repeat the same matrix here, keep the detailed grading with the central reference on material selection — it lists the acceptance numbers and sampling levels our team works to.
Where this build route is strongest
Packing film-laminated panels without blocking or creasing
A welded or film-laminated panel behaves nothing like a plain woven polyester shell once it is closed inside a carton. The coating face is thermoplastic, so under the heat and pressure of a stacked container it can block, pick up print from the panel next to it, or keep a permanent crease along a fold line. QUANZHOU JUNYUAN BAGS treats packing as part of the product specification rather than a warehouse decision, and the packing clause is written into the same document that carries weld width, hydrostatic target and the AQL 2.5 acceptance level.
Blocking is driven by three variables: coating softening point, stack pressure and dwell time. A TPU laminate with a softening point near 120 degrees Celsius will normally survive a 25 to 35 day sea voyage without marking, while a PVC-backed shell can start to transfer at contact points when a carton sits under eight layers of load for weeks. The working rule for coated styles is a maximum of six cartons per pallet layer, a barrier sheet placed coated face to coated face between units, and no fold placed across a welded seam.
Each unit goes into a 0.04 mm LDPE polybag with two 6 mm vent holes per side so residual solvent and moisture can escape instead of condensing on the film face. Silica gel is loaded at one 5 g sachet per 0.03 cubic metre of carton volume, which is enough for a full container run without overdrying the coating. Cartons are five-ply BC flute with a minimum burst strength of 1,100 kPa, and the packed carton is qualified to ISTA 3A before the first bulk shipment leaves.
Retail presentation, labelling and container planning
Retail-ready packing adds a separate layer of requirements. A pegged unit needs an EAN-13 barcode printed with a quiet zone that is not folded over the hook hole, and the symbol must still reach a scan grade of at least 2.5 after the carton has been through transit. Fulfilment-bound shipments need a scannable unit label on every piece and a master carton that stays under 22.5 kg unless it is marked as team lift, because a heavier carton is refused at most receiving docks.
| Packing element | Specified value | Reason it is controlled |
|---|---|---|
| Polybag gauge | 0.04 mm LDPE, vented | Stops condensation marking the coating |
| Desiccant loading | 5 g per 0.03 cubic metre | Covers a 25 to 35 day container voyage |
| Carton board | Five-ply BC, 1,100 kPa burst | Survives six-layer pallet stacking |
| Master carton weight | Under 22.5 kg | Avoids team-lift refusal at the dock |
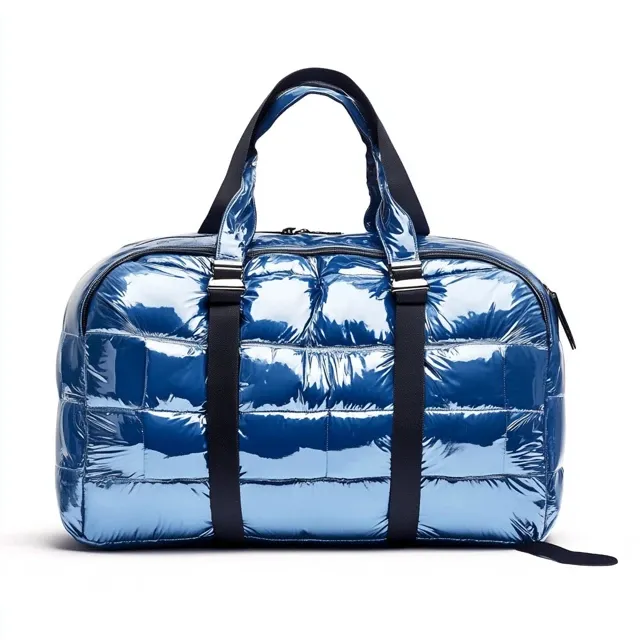
Carton cube then decides freight cost. A 40 litre welded duffel packed flat consumes roughly 0.045 cubic metre per unit, so a 40HQ at 68 CBM carries about 1,500 pieces before pallet allowance, while a 20GP at 28 CBM carries roughly 600. Brands that specify retail cartons early avoid the common surprise of a season order that fills the container long before it reaches the weight limit.
Packing is verified at the same checkpoint as the product itself: carton count, marking data and barcode readability are checked against the packing list before the truck departs for the port under the quality certification protocol, and the same spec feeds the export documentation set.
Frequently Asked Questions (FAQs)
Why does a coated panel block together inside a sealed export carton?
Blocking happens when the thermoplastic coating face softens under stack pressure and long dwell time. A PVC-backed shell can mark at contact points after eight carton layers over a 25 to 35 day voyage, so coated styles are limited to six layers with a barrier sheet between units.
What polybag gauge and venting suit a film-laminated panel on a sea voyage?
A 0.04 mm LDPE polybag with two 6 mm vent holes per side is specified. Venting lets residual solvent and moisture escape instead of condensing on the film face, which would otherwise show as clouding when the carton is opened at destination after 25 to 35 days at sea.
How many welded-seam duffels should be stacked per pallet layer before seam creep?
Six cartons per layer is the limit for coated and welded styles. Beyond that the cumulative load presses the weld line and the seam creeps, which shows as a wavy closure or a narrowed weld width. The carton board is specified at 1,100 kPa burst to hold that stack.
How much silica gel does a container of coated bags actually need?
The loading is one 5 g sachet per 0.03 cubic metre of carton volume. A 40HQ at 68 CBM therefore needs roughly 2,260 sachets spread across the shipment. Underdosing leaves condensation on the film face, while overdosing can dry a PU coating beyond its intended hand feel.
Where should an EAN-13 retail barcode sit so it still scans on a peg hook?
The symbol needs its full quiet zone clear of the hook hole and clear of any fold. Print placement is dimensioned in millimetres on the hangtag artwork, and the code is verified at a minimum ANSI scan grade of 2.5 after transit simulation, not only at the printer.
What carton board and burst strength carry a coated bag through ISTA 3A?
Five-ply BC flute with a minimum burst strength of 1,100 kPa is the baseline for a 25 to 35 day sea transit from Xiamen. The packed carton is then qualified to ISTA 3A before the first bulk run ships, covering drop, vibration and compression in a single sequence.
Should retail inner packs be sealed or perforated for a coated product?
Perforated inner packs are used for coated styles. A fully sealed inner pack traps moisture against the film face and accelerates blocking over a 25 to 35 day voyage, while a perforated pack keeps air moving through the stack. Perforations are specified at 6 mm spacing, roughly 20 per pack, alongside the polybag gauge.
How much container volume does one 40 litre welded duffel consume?
A 40 litre welded duffel packed flat consumes about 0.045 cubic metre, so a 40HQ at 68 CBM holds roughly 1,500 units and a 20GP at 28 CBM holds about 600 before pallet allowance. Cube, not weight, is what fills the container on this product type.
Further Reading and Internal Resources
Internal resources
Related blog posts
- How to Transition From ODM to Full OEM Bag Production
- Incoming Material Inspection (IQC) for Bag Factories
- How to Test Waterproof Bag Performance (Factory Standards)
- How to Track Your Bag Order From Factory to Port
- How to Shorten Bag Production Lead Times Without Risks
- How to Test Cooler Bag Ice Retention (Factory Standards)
Next step
• Lock keyword and claim scope for custom waterproof bag oem
• Build a tech pack with BOM + tolerance map
• Choose materials route and validate tests (by spec)
• Plan sampling gates (lead time 6-10 working days)
• Set MOQ and cost targets (MOQ 500 pcs)
• Define QC plan and AQL checkpoints
• Confirm production + shipping timeline (35-50 days)
Ready to move on your next build?
Send over your requirements; a manufacturing plan and structured RFQ checklist are prepared for you.
Next guides: custom backpacks.
Packing specification, carton maths and what damages film in transit
Waterproof construction creates a packing problem most programmes discover too late: a bag that holds water out also holds moisture in. Sealing a freshly welded shell in a polybag the same day it comes off the line traps humidity against the film, and four weeks later the last thing the receiving team expects to see — spotting inside a supposedly watertight product — is exactly what they find. Packaging decisions for these lines are therefore part of the product specification, not an afterthought for the logistics department.
The first requirement is conditioning. Allow at least 24 hours for goods to reach ambient humidity before bagging, and specify that plainly in the packing instruction rather than assuming it. Desiccant should be sized to the carton rather than to habit: a 5 gram sachet is adequate for a small carton in a dry season, 10 grams above roughly 60 percent relative humidity at loading, and both should be recorded on the packing instruction alongside a note that the sachet should not sit directly against a printed logo, since concentrated desiccant dust can mark some finishes.
The second is protecting the film surface. TPU and PVC faces abrade against each other and against raw carton board, and unlike fabric they cannot be steamed or brushed back. Use interleaving between folded faces, specify a carton with at least 32 ECT bursting strength for a 20-foot container load stacked four high, and never allow direct contact between a printed face and a waxed surface. Where a bag ships flat-folded, roll it around a soft core rather than creasing it twice, since repeated hard folds set a memory into heavier laminates.
| Element | Specification | Damage prevented |
|---|---|---|
| Conditioning | 24 hours at ambient before bagging | Internal condensation and spotting |
| Desiccant | 5 g standard, 10 g above 60% RH | Mould growth across a long sea leg |
| Interleaving | 35–40 gsm acid-free tissue at every fold | Face-to-face abrasion and print transfer |
| Inner bag | 0.04–0.05 mm LDPE, six 6 mm vent holes | Trapped humidity without a dust path |
| Carton strength | 32 ECT minimum, double wall above 18 kg | Stack collapse in a 40HQ |
| Pallet pattern | Interlock, stretch-wrapped, corner board at four edges | Shift damage and crushed corners |
| Carton marks | SKU, colourway, quantity, carton n of N, net and gross weight | Receiving disputes and miscounts |
Working the freight numbers before you freeze the design
Container utilisation belongs in the design review, because it often costs more than a component change. Use 28 CBM for a 20GP, 56 for a 40GP and 68 for a 40HQ, and run the calculation both ways: a pack that ships flat may fill a 40HQ at 2,400 units while the same bag with a moulded base may not exceed 900, which turns a freight saving into a per-unit penalty larger than most material savings. Ask for a packed-dimension estimate at sampling rather than at booking.
Transit mode should also be chosen deliberately. Sea freight at 25 to 35 days is the default for cost, but it exposes film goods to container temperatures that can exceed 60 °C, which is precisely when blocking and migration problems begin. If your launch date is inside eight weeks, quote the programme on air at 5 to 8 days or courier at 3 to 5 rather than discovering at week ten that the cheapest lane is the reason the goods arrived damaged. Remember that FOB Xiamen under Incoterms 2020 covers the export leg only; CIF and DDP quotes put the whole figure on one line if you prefer that.
Master carton weight limits matter more than they appear to. Keeping individual cartons under about 18 kg reduces manual handling damage, keeps them compliant with common warehouse handling policies, and prevents the crushed-bottom-corner pattern that appears when heavy cartons are dragged rather than lifted. Where unit weight pushes the carton over that threshold, split the quantity rather than upgrading board spec, since splitting is usually cheaper than heavier board.
Finally, plan the retail side early. A hangtag on a waterproof product is a puncture risk if it is pinned through the shell, so use a loop through a webbing point or a removable adhesive tab. Silica packets inside the retail bag protect display stock but need a statutory child-safety warning in several markets. Labelling and barcodes must be agreed before packing begins, since applying them afterwards costs more than applying them in line. Raise all of it with us at contact, or read more background in our technical guides.
Numbers age badly when copied into dozens of places, so the maintained version of this grid stays on quality control and certification.
Rather than repeat the same matrix here, keep the detailed grading with the central reference on material selection — it lists the acceptance numbers and sampling levels our team works to.